Bulk Cable Assembly Orders: How to Reduce Shipping and Delay Risks
- Building a Predictable High-Volume Connectivity Supply Plan
- Freeze the technical definition before requesting volume pricing
- Approve a golden sample and retain measurable acceptance criteria
- Match supplier capacity to the real production profile
- Controlling Manufacturing, Packaging, and Export Exposure
- Use lot traceability and staged quality gates
- Design packaging around connector geometry and transit conditions
- Prevent customs and documentation delays
- Reducing Delay Consequences Through Logistics Planning
- Segment shipments according to project criticality
- Build schedule buffers from actual process variability
- Define a receiving and installation readiness protocol
- Why WEIPU Supports Lower-Risk Industrial Connector Programs
- Scale, specification breadth, and standards knowledge
- Vertically integrated production for better schedule control
- Performance options for mission-critical applications
- Frequently Asked Questions
Bulk cable assembly orders require more than a low unit price: buyers must control technical variation, production readiness, packaging integrity, export documentation, transit exposure, and final-site installation timing. The most effective risk-reduction model combines a frozen bill of materials, approved samples, supplier capacity verification, lot traceability, shipment segmentation, compliant customs data, and a contingency plan for critical industrial connectors. For demanding applications, a vertically integrated manufacturer can shorten handoffs and improve delivery predictability across circular, heavy-duty, CEE, medical, renewable-energy, rail, and smart-manufacturing programs.
Building a Predictable High-Volume Connectivity Supply Plan
Freeze the technical definition before requesting volume pricing
Many delivery failures begin before production starts. A purchase order may describe a connector family but omit contact plating, conductor cross-section, cable jacket material, bend radius, pin assignment, shielding method, operating temperature, ingress-protection requirement, or mating-cycle target. Each missing variable creates room for supplier interpretation, engineering changes, and rework.
Buyers should issue a controlled technical package containing the approved drawing, wiring schedule, connector part numbers, cable specification, terminal requirements, length tolerance, labeling format, inspection criteria, applicable regulatory requirements, and revision level. The document should distinguish mandatory characteristics from allowable substitutions. If a project uses a circular connector in vibration, washdown, or outdoor service, the specification should state the environmental exposure and required protection rating rather than relying on a generic product name.
A configuration-control process is equally important. Every engineering change should have an effective date, affected purchase-order lines, sample-approval status, and disposition for existing inventory. This prevents mixed revisions from reaching the same installation site, where technicians may lose time identifying incompatible pinouts or mechanical interfaces.
Approve a golden sample and retain measurable acceptance criteria
A production sample should represent the final material, tooling, labeling, overmolding, strain relief, and test sequence. Approval should not be based only on appearance. The buyer and supplier should record continuity, insulation resistance, dielectric withstand where applicable, contact retention, pull force, dimensional checks, torque values, and visual workmanship requirements.
The approved reference unit becomes a practical boundary for quality decisions. It also supports faster dispute resolution because the parties can compare a questioned lot against a documented standard. For repeat programs, a digital photograph set, inspection report, and serialized sample record can reduce ambiguity between purchasing, engineering, quality, and logistics teams.
Match supplier capacity to the real production profile
Annual capacity alone does not guarantee on-time delivery. Procurement teams should examine monthly output, line loading, tooling availability, critical raw-material lead times, quality release queues, and the supplier’s ability to support demand spikes. A manufacturer may have adequate total capacity but insufficient molding machines, crimping stations, test fixtures, or trained operators for a particular connector family.
Ask for a capacity plan that separates standard items, customized components, and long-lead materials. The plan should show purchase-order milestones, first-article approval, pilot build, mass production, final inspection, packing completion, and dispatch readiness. A supplier scorecard can track on-time-in-full performance, first-pass yield, corrective-action closure, response time, and documentation accuracy.
Controlling Manufacturing, Packaging, and Export Exposure
Use lot traceability and staged quality gates
High-volume cable harness production should be divided into identifiable lots tied to raw materials, operators or work centers, tooling, inspection results, and shipment cartons. Traceability enables targeted containment if a defect is discovered instead of forcing a complete project-wide quarantine.
Quality gates should occur at incoming material inspection, conductor preparation, crimp or termination, connector installation, electrical testing, visual inspection, and final packing. Automated continuity and pinout testing is particularly valuable for multi-branch harnesses because a wiring reversal can remain invisible during a simple visual check. Test records should identify the harness or lot, not merely provide an unlinked pass certificate.
For quality-system alignment, buyers can evaluate the supplier against the principles of ISO 9001 quality management. The standard does not guarantee a specific delivery date, but its process approach helps buyers assess documented controls, corrective action, customer requirements, and continual improvement.
Design packaging around connector geometry and transit conditions
Shipping damage is often caused by packaging designed for cable length rather than connector mechanics. Heavy plugs can pull against overmolds, exposed contacts can be contaminated, and tight coil radii can create permanent deformation. Packaging should use protective caps, separators, moisture barriers where required, and bend-radius controls. Each carton should identify part number, revision, quantity, lot, gross weight, net weight, carton sequence, and handling orientation.
Cartonization should be validated through practical handling and, for sensitive programs, formal distribution testing. The packaging plan must account for pallet stacking, container vibration, temperature changes, humidity, and repeated loading. Desiccant and corrosion protection may be necessary for metallic contacts moving through humid routes, but these materials should not contact sensitive surfaces in a way that creates contamination.
Prevent customs and documentation delays
International shipments can be delayed by inconsistent commercial invoices, incorrect quantities, ambiguous product descriptions, missing origin data, or mismatched packing lists. The supplier and buyer should agree in advance on the harmonized tariff classification, country-of-origin treatment, Incoterm, consignee details, export-control screening, and document owner. The World Customs Organization Harmonized System is the internationally recognized basis for classifying traded goods, but the final declaration should be confirmed with the responsible customs broker and importing authority.
Incoterms should be selected for operational clarity rather than habit. The International Chamber of Commerce Incoterms rules define responsibilities, costs, and risk transfer between seller and buyer; they do not replace a complete logistics plan. Purchase orders should state who books transport, who provides insurance, who handles import clearance, and who pays duties or destination charges.
| Risk area | Weak control | Recommended control | Buyer outcome |
|---|---|---|---|
| Technical variation | Uncontrolled email changes | Revision-controlled drawing and approved golden sample | Fewer mismatched or obsolete units |
| Production timing | Single promised ship date | Milestone plan with capacity and quality-release dates | Earlier visibility of slippage |
| Transit damage | Generic cartons and loose coils | Connector-specific separators, caps, and bend-radius protection | Lower receiving defects |
| Customs clearance | Incomplete or inconsistent documents | Pre-validated classification, invoice, packing list, and origin data | Reduced border-hold exposure |
| Schedule continuity | One shipment for all material | Phased dispatches and a prioritized allocation plan | Critical installation work can start sooner |
Reducing Delay Consequences Through Logistics Planning
Segment shipments according to project criticality
A single full-volume dispatch may appear efficient, but it concentrates risk. If a container is rolled, held at customs, damaged, or misrouted, the entire installation may stop. A better approach is to classify items as commissioning-critical, production-critical, standard replenishment, and non-critical spares. Ship the first two categories earlier or through a faster service while moving stable, non-urgent quantities through the lowest total-cost route.
Shipment segmentation should not create uncontrolled partial deliveries. Each release needs a packing list, installation priority, minimum usable quantity, and receiving contact. Buyers should also verify whether the site can store moisture-sensitive products safely and whether partial deliveries create extra handling or inventory-counting costs.
Build schedule buffers from actual process variability
A schedule buffer should reflect engineering approval time, material procurement, manufacturing, inspection, export handling, transportation, import clearance, and site receiving. Adding an arbitrary number of days is less useful than identifying the longest and most variable steps. Customized overmolds, special cable jackets, nonstandard plating, and large connector combinations often require more planning than catalog items.
Use milestone alerts rather than waiting for the final dispatch notice. Useful triggers include drawing approval, material availability, tooling completion, pilot acceptance, production start, 50% completion, final test release, packing completion, and carrier pickup. Escalation rules should specify when the supplier must propose overtime, alternate transport, split delivery, or an approved equivalent.
Define a receiving and installation readiness protocol
On-site delay can occur even when the shipment arrives on time. The receiving team should have the purchase order, carton map, inspection checklist, test equipment, storage instructions, and installation drawings before delivery. For complex harnesses, labels should correspond to the wiring schedule and equipment tags used by technicians.
Incoming inspection should verify carton count, part number, revision, lot, connector condition, cable length, pinout, and visible damage. Any nonconformance should be photographed and isolated by lot. This process protects the project from installing a questionable batch and gives the manufacturer actionable evidence for rapid resolution.
Why WEIPU Supports Lower-Risk Industrial Connector Programs
Scale, specification breadth, and standards knowledge
WEIPU has operated since 1996 and is a global supplier of high-reliability industrial connectors. As a principal drafter of the GB/T 11918-2014 national standard, our engineering and manufacturing organization understands the importance of mechanical fit, electrical performance, environmental protection, and consistent product definition in demanding connectivity programs.
Our 2025 expansion has scaled the facility to 80,000 m² and supports annual capacity of 55 million units. More than 70,000 specifications cover circular connector, heavy-duty connector, CEE connector, and other industrial connector requirements. This breadth helps buyers consolidate sourcing while preserving the ability to match connector geometry, current rating, environmental conditions, and installation method to the application.
Vertically integrated production for better schedule control
Our independent R&D capability and vertically integrated production system reduce unnecessary handoffs between design, tooling, manufacturing, testing, and logistics. A one-stop approach can simplify technical clarification, reduce duplicated approvals, and create a clearer escalation path when a project requires a controlled modification.
WEIPU supports OEM and ODM programs with a 24-hour rapid-response model and prototype delivery in 7–15 days, subject to design complexity and approval requirements. Early prototypes allow project owners to validate mating, routing, clearance, sealing, ergonomics, and installation workflow before committing to a large production release. That early validation is one of the most effective ways to prevent expensive late-stage rework.
Performance options for mission-critical applications
Our product technology includes IP69K protection options, high-current solutions up to 800A, and medical connectivity designed to withstand 134°C autoclaving. These capabilities support harsh washdown environments, high-power systems, sterilizable medical equipment, renewable-energy installations, rail transit, and smart-factory machinery. Buyers should still confirm the exact product rating, test method, cable construction, and application conditions for each project rather than generalizing from a family-level specification.
WEIPU holds IRIS certification for rail transit and IATF 16949 certification for automotive applications. These credentials, together with documented engineering and quality processes, give procurement teams a stronger basis for supplier qualification. WEIPU serves more than 30,000 customers across 130 countries, providing the international logistics familiarity needed for multi-site programs and distributor replenishment.
For a bulk release, our team can support specification review, sample approval, product selection, packaging definition, OEM/ODM coordination, production planning, and export documentation alignment. The objective is not simply to manufacture more units; it is to deliver the right configuration, in identifiable lots, with packaging and documentation that support fast receiving and dependable installation.
For technical references, buyers may also consult the International Electrotechnical Commission standards framework and the ISO 13849-1 safety-related control systems standard when evaluating equipment-level connectivity and machinery risk requirements. Product selection must remain application-specific and should be confirmed through the applicable project standards, drawings, and validation tests.
Contact WEIPU at salse01@weipu-group.com or +86-020-80501102 to review your volume requirements, technical package, packaging plan, and delivery milestones, or visit https://www.weipu-group.com/ to explore industrial connector solutions.
Frequently Asked Questions
How can buyers prevent specification errors in bulk cable assembly orders?
Buyers should issue a controlled technical package containing the approved drawing, wiring schedule, connector part numbers, cable specification, terminal requirements, length tolerance, labeling format, inspection criteria, applicable regulatory requirements, and revision level. An approved golden sample should also represent the final materials, tooling, labeling, overmolding, strain relief, and test sequence.
What should be included in a supplier capacity plan?
A supplier capacity plan should show monthly output, line loading, tooling availability, critical raw-material lead times, quality release queues, trained-operator capacity, purchase-order milestones, first-article approval, pilot build, mass production, final inspection, packing completion, and dispatch readiness.
How should industrial connector products be packaged for international shipping?
Packaging should use protective caps, separators, moisture barriers where required, and bend-radius controls. Each carton should identify the part number, revision, quantity, lot, gross weight, net weight, carton sequence, and handling orientation. The design should account for pallet stacking, container vibration, temperature changes, humidity, and repeated loading.
Why are phased shipments useful for large connector programs?
Phased shipments reduce concentrated risk. Items should be classified as commissioning-critical, production-critical, standard replenishment, or non-critical spares. Critical categories can move earlier or through faster transport, while stable non-urgent quantities use the lowest total-cost route.
What documents help prevent customs clearance delays?
The supplier and buyer should agree in advance on the harmonized tariff classification, country-of-origin treatment, Incoterm, consignee details, export-control screening, and document owner. The commercial invoice, packing list, quantities, product descriptions, and origin data should remain consistent.
What quality records should accompany high-volume harness production?
Lots should be tied to raw materials, work centers, tooling, inspection results, and shipment cartons. Quality gates should cover incoming materials, conductor preparation, crimping or termination, connector installation, electrical testing, visual inspection, and final packing. Test records should identify the harness or lot.
What makes WEIPU suitable for bulk industrial connector programs?
WEIPU provides more than 70,000 specifications, an 80,000 m² facility, annual capacity of 55 million units, OEM/ODM services, 24-hour rapid response, and prototype delivery in 7–15 days. The company supports circular, heavy-duty, CEE, medical, renewable-energy, rail, and smart-manufacturing applications and holds IRIS and IATF 16949 certifications.
Customizable Professional Socket with Cap: Options for OEMs
Installation Best Practices for Clamping Plates in Harsh Environments
Contact Types and Pin Configurations: Circular Connector Options
Waterproof Connector Lead Times, Shipping, and Buffer Stock Planning

SY1110/P SY1110/S Cable connector IP67
Mate with SP1111,SP1112

WEIPU SP1110P/S Cable Connector IP68
Mate with SP1111, SP1112
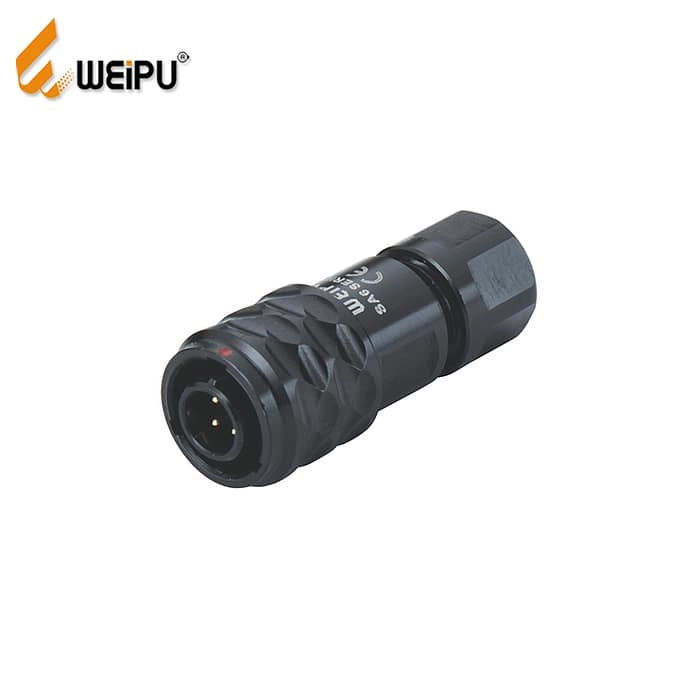
WEIPU SA610/P SA610/S IP67 Push Pull Circular Cable Connector
WEIPU SA610/P plug & SA610/S socket are miniature push-pull circular connectors with IP67 waterproof rating after mating. Built with anodized aluminum shell and gold-plated solder contacts, this SA series supports 2-5 pins, rated 3A 30V, certified CE & RoHS. Ideal for medical diagnostic devices, lab automation and precision sensors, fully compatible with SA611, SA612 and SA615 panel receptacles. WEIPU holds IATF16949 certification and supplies industrial connectors to 130+ countries.

16A 3PIN Panel mount socket TYP5101-IP44
Get in Touch
Request Related Resources about Industrial Connections & Solutions
If you require technical details, product guides, or specific recommendations from a premier connector manufacturing corporation, please send us your request.
We provide expert support for custom electrical connectors, offering OEM/ODM customization and dedicated distributor cooperation assistance.
Weipu Building, No. 111, Baihua Road, Liwan District, Guangzhou, Guangdong China
© 2026 WEIPU. All Rights Reserved.
Whatsapp: +8618102298073
WEIPU
WEIPU
WEIPU
WEIPU