Chrome-Plated vs Nickel-Plated Zinc Alloy Industrial Connectors
Comparative technical analysis and procurement guidance on chrome-plated zinc alloy industrial connectors vs nickel-plated zinc alloy industrial connectors, covering corrosion resistance, wear and abrasion, electrical contact behavior, environmental compliance, lifecycle cost, inspection criteria, and application mapping for circular connectors, heavy-duty connectors, and industrial connector assemblies used in rail, automotive, medical, and renewable energy sectors; includes a data comparison table, verifiable standards references (Electroplating, ISO, IEEE Standards, IEC), and a practical supplier checklist for spec writers and procurement teams.
- Surface Finish Performance: Corrosion, Hardness, and Wear
- Electrochemical resistance and environmental behavior
- Hardness, abrasion, and mating cycles
- Electrical contact and conductivity considerations
- Procurement & Specification: Risk Mitigation and Test Criteria
- Standards, test methods, and acceptance criteria
- Manufacturing process controls and QA checkpoints
- Total cost of ownership and lifecycle analysis
- Application Mapping: When to Specify Chrome vs Nickel
- High-wear and high-cycle environments
- Corrosive and marine applications
- Appearance, color, and branding requirements
- Data-Driven Comparison
- Supplier Checklist and Due Diligence
- Requested documentation and samples
- Compliance, environmental, and regulatory screening
- Inspection acceptance and production release
- WEIPU Capabilities and Why Supplier Selection Matters
- Manufacturing scale, standards, and vertical integration
- Certifications, technical benchmarks, and product range
- Supply reliability, customization, and service model
- Frequently Asked Questions
Chrome plating and nickel plating are two commonly specified surface finishes for zinc alloy connector shells; choosing between a chrome-plated zinc alloy industrial connector and a nickel-plated zinc alloy industrial connector requires evaluating electrochemical behavior, plating thickness, hardness, solderability, and life-cycle maintenance costs. This technical brief synthesizes material science, test-method outcomes, and procurement criteria to help buyers select the optimal surface treatment for circular connectors, heavy-duty connectors, and other industrial connector formats used across transportation, renewable energy, manufacturing automation, and medical devices.
Surface Finish Performance: Corrosion, Hardness, and Wear
Electrochemical resistance and environmental behavior
Nickel plating typically provides a continuous, ductile barrier layer that is effective against uniform corrosion and is commonly specified with thicknesses in the range of 5–25 µm for protective coatings on zinc alloy substrates. A chrome-plated zinc alloy industrial connector often uses a thin decorative or hard chrome topcoat over a nickel underlayer; hard chrome increases surface hardness and abrasion resistance but may be thinner (sub-micrometer to low-micrometer range) in decorative applications. For outdoor or marine environments, procurement teams should prioritize overall system corrosion protection—this usually favors nickel as the primary corrosion barrier, with chrome used where additional surface hardness or aesthetic brightness is required. See electrochemical fundamentals at Electroplating.
Hardness, abrasion, and mating cycles
Hard chrome offers elevated surface hardness and thus better abrasion resistance under frequent mating/demating cycles, which benefits certain heavy-duty connectors that face mechanical wear. However, chrome’s brittleness compared with nickel can result in cracking over sharp edges or in high-flex areas. For connectors subjected to frequent coupling cycles or abrasive contaminants, a chrome-plated zinc alloy industrial connector with a robust nickel underplate commonly provides the best compromise: nickel for ductility and corrosion resistance, chrome for surface hardness where required.
Electrical contact and conductivity considerations
Plating on non-conductive shell areas generally does not affect signal integrity, but contacts and contact regions must consider solderability, contact resistance, and galvanic coupling. Nickel layers can increase contact resistance if overly thick; passivation layers and post-plating treatments mitigate this. When connector shell bonding to chassis or EMC bonding is required, ensure the specification identifies unplated or properly prepared bonding surfaces. For designs where contact plating is integrated into the shell interface, the chrome-plated zinc alloy industrial connector should be validated for acceptable contact resistance over the expected lifecycle and environmental conditions.
Procurement & Specification: Risk Mitigation and Test Criteria
Standards, test methods, and acceptance criteria
Specify standard test methods in purchase orders: salt spray (ASTM B117 or ISO 9227 equivalents), adhesion pull tests, microhardness, and cyclic corrosion tests where applicable. Refer to normative sources such as ISO and IEC for environmental and electrical test standards. Establish acceptance limits (e.g., no red rust in 96–240 hours for zinc substrates where required) and require supplier test reports that identify plating thickness, bath chemistry (trivalent chromium vs hexavalent chromium concerns), and process controls.
Manufacturing process controls and QA checkpoints
Request detailed process flow: substrate preparation, activation, nickel strike, nickel build-up, optional flash coatings, and chrome deposition details. Critical control points include plating thickness measurement (XRF), adhesion (cross-hatch and pull tests), and bath composition traceability. For mission-critical projects, require sample verification reports, production run capability metrics, and failure-mode analysis documentation in the supplier quality plan.
Total cost of ownership and lifecycle analysis
Unit plating cost differences are usually modest; however, the true cost analysis must factor replacement intervals, maintenance, warranty exposure, and end-of-life recycling costs. A chrome-plated zinc alloy industrial connector may present higher initial finishing costs (if a hard chrome topcoat is specified) yet reduce wear-related failures; a nickel-plated connector may reduce corrosion-related replacements. Procurement teams should perform a simple NPV comparison across projected failure rates and service intervals to determine the more economical long-term option.
Application Mapping: When to Specify Chrome vs Nickel
High-wear and high-cycle environments
For industrial connectors exposed to mechanical abrasion, particulate ingress, or repeated coupling—such as connectors on factory robots, heavy machinery, and outdoor renewal energy junctions—a chrome-plated zinc alloy industrial connector with a controlled nickel underplate can extend service life by combining hardness and base protection. Where dust or abrasive contaminants are present, evaluate IP ratings (IP67/68/69K) and mating surface protection strategies.
Corrosive and marine applications
In coastal, salt-spray, or chemically aggressive environments the corrosion barrier is paramount. Nickel-plated zinc alloy industrial connectors specified with thicker nickel deposits, proper sealing, and corrosion-resistant gaskets will typically outperform thin chrome topcoats that rely on a nickel underlayer for corrosion protection. Ensure that salt-spray and cyclic corrosion testing is part of the qualification protocol.
Appearance, color, and branding requirements
Where aesthetics and surface gloss are specification drivers (front-panel components, visible housings), chrome finishes provide a bright, mirror-like surface suitable for product branding. Buyers should confirm that the decorative chrome is applied over a nickel underplate engineered to the corrosion resistance required by the end-use environment; otherwise, bright chrome alone will not provide long-term protection for zinc alloys.
Data-Driven Comparison
| Property | Chrome-Plated Zinc Alloy | Nickel-Plated Zinc Alloy | Typical Application Notes |
|---|---|---|---|
| Plating structure | Thin chrome topcoat over nickel underplate (chrome 0.2–2 µm; nickel varies) | Continuous nickel layer (typically 5–25 µm) | Chrome often used for hardness/appearance; nickel for barrier protection |
| Corrosion resistance | Depends on nickel underlayer; alone offers limited corrosion protection | Superior as primary corrosion barrier (thicker deposit improves performance) | Nickel preferred for marine/external use |
| Surface hardness | High (hard chrome increases abrasion resistance) | Moderate; ductile and less prone to cracking | Chrome wins for wear; nickel for ductility |
| Solderability / electrical contact | Potentially problematic on contact surfaces; needs design-specific treatment | Better controlled for contact areas; can be post-treated | Specify non-plated bonding/solder areas if required |
| Typical cost impact | Higher if chrome hardcoat added; decorative chrome increases process steps | Moderate; standard plating line capability | Assess lifecycle cost, not only unit price |
Supplier Checklist and Due Diligence
Requested documentation and samples
Require plating thickness reports (XRF), salt spray / cyclic corrosion test certificates, adhesion and hardness test data, process control flow, and material traceability for the zinc alloy substrate. Request representative samples for mating-cycle testing and electrical validation in the intended assembly to confirm that a chrome-plated zinc alloy industrial connector or nickel-plated zinc alloy industrial connector meets the project acceptance criteria.
Compliance, environmental, and regulatory screening
Confirm plating bath chemistry complies with local and international restrictions (e.g., hexavalent chromium regulations). For rail or automotive applications require supplier certifications aligned with industry standards; consult IEEE Standards and relevant industry norms. Include end-of-life and RoHS/REACH declarations when required by contract.
Inspection acceptance and production release
Define in the purchase order the acceptance sampling, destructive testing quotas, and non-conformance remediation process. For high-volume deployments, require ongoing process capability metrics and periodic audit access to the supplier’s plating lines to ensure consistent application—critical when specifying a chrome-plated zinc alloy industrial connector with thin topcoats that are sensitive to process variation.
WEIPU Capabilities and Why Supplier Selection Matters
Manufacturing scale, standards, and vertical integration
Founded in 1996, WEIPU is a global leader in high-reliability industrial connectors and a principal drafter of the GB/T 11918-2014 national standard. With nearly 30 years of expertise, our 2025 expansion has scaled our facility to 80,000 m², supporting an annual capacity of 55 million units. Our independent R&D and vertically integrated production system minimize variability in plating and finishing processes, ensuring consistent application whether specifying a chrome-plated zinc alloy industrial connector, a nickel-plated zinc alloy industrial connector, or other finishes across circular connector, industrial connector, and Heavy Duty Connector product families.
Certifications, technical benchmarks, and product range
WEIPU supports procurement teams with elite IRIS (Rail Transit) and IATF 16949 (Automotive) aligned processes, demonstrating compliance with stringent global safety standards. Our technology benchmarks include IP69K protection, 800A high-current capability, and medical-grade solutions resistant to 134°C autoclaving. Buyers can select from over 70,000 specifications—including circular connector, industrial connector, and Heavy Duty Connector formats—backed by production controls that document plating chemistry, thickness, adhesion, and lifecycle test results.
Supply reliability, customization, and service model
WEIPU offers a one-stop solution with 24-hour rapid response and OEM/ODM services, delivering prototypes in 7–15 days. For projects where the choice between a chrome-plated zinc alloy industrial connector and a nickel-plated zinc alloy industrial connector is material to system performance, our engineering team provides material selection guidance, sample validation, and production verification to align finish selection with environmental exposure, mating cycles, and electrical requirements. Procurement teams receive full documentation, test certificates, and post-delivery support to minimize field failures and warranty claims.
Contact WEIPU for technical datasheets, plating process documentation, or to request qualification samples; visit WEIPU, email salse01@weipu-group.com, or call +86-020-80501102.
Frequently Asked Questions
What are the primary functional differences between chrome-plated and nickel-plated zinc alloy connectors?
Chrome plating delivers high surface hardness and improved abrasion resistance, often applied as a thin topcoat over nickel; nickel plating provides a more ductile, continuous corrosion barrier (typically 5–25 µm). For long-term corrosion protection, nickel is generally preferred; for wear resistance and appearance, chrome over nickel may be selected.
Which finish is better for outdoor or marine environments?
Nickel-plated zinc alloy connectors with sufficient thickness and proper sealing are typically better for outdoor or marine environments because nickel provides a more reliable corrosion barrier. Chrome finishes that rely on a thin topcoat require a robust nickel underlayer to perform acceptably in corrosive conditions.
How should procurement teams specify tests for plating acceptance?
Include salt spray (ISO 9227/ASTM B117 equivalents), adhesion, plating thickness (XRF), hardness, and cyclic corrosion tests where applicable. Require supplier test reports that show bath chemistry, plating thickness ranges, and sample test results. Define acceptance limits and non-conformance actions in the PO.
Can chrome or nickel plating affect electrical contact or solderability?
Yes. Thick nickel layers can increase contact resistance; chrome topcoats can impede solderability. Specify unplated or specially treated bonding/solder areas where electrical continuity or soldering is required, and validate contact resistance through lifecycle testing.
What are key contractual clauses to reduce finish-related risks?
Require process flow documentation, XRF plating thickness reports, regular quality metrics, production samples, and rights to audit. Include warranty periods tied to defined environmental exposures and mandate corrective action timelines for plating-related failures.
Case Studies: Distribution Box Solutions by Industry
Cost Factors: What Affects Distribution Box Pricing

WY-ZE Series Waterproof Circular Power Connector IP67 — Reliable Industrial Power Connections
Gland Cable Selection for Distributors, OEMs, and Project Buyers

SY1110/P SY1110/S Cable connector IP67
Mate with SP1111,SP1112

WEIPU SP1110P/S Cable Connector IP68
Mate with SP1111, SP1112
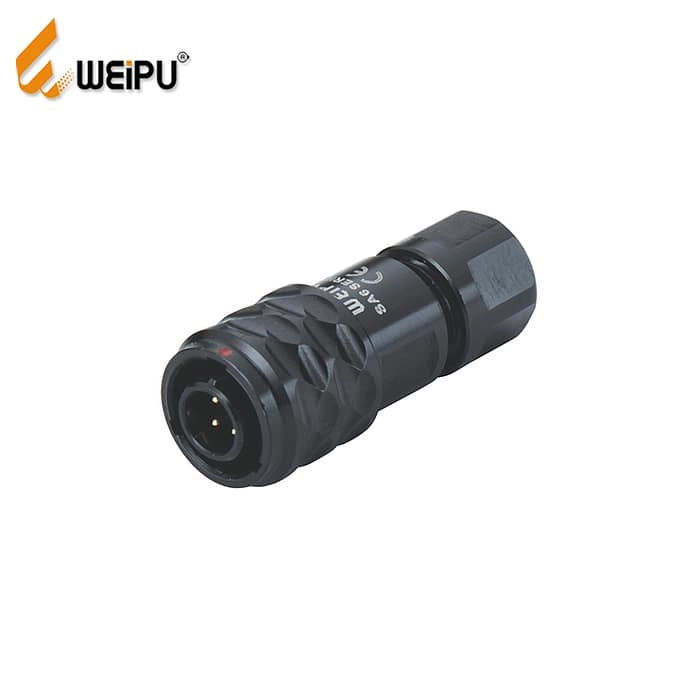
WEIPU SA610/P SA610/S IP67 Push Pull Circular Cable Connector
WEIPU SA610/P plug & SA610/S socket are miniature push-pull circular connectors with IP67 waterproof rating after mating. Built with anodized aluminum shell and gold-plated solder contacts, this SA series supports 2-5 pins, rated 3A 30V, certified CE & RoHS. Ideal for medical diagnostic devices, lab automation and precision sensors, fully compatible with SA611, SA612 and SA615 panel receptacles. WEIPU holds IATF16949 certification and supplies industrial connectors to 130+ countries.

16A 3PIN Panel mount socket TYP5101-IP44
Get in Touch
Request Related Resources about Industrial Connections & Solutions
If you require technical details, product guides, or specific recommendations from a premier connector manufacturing corporation, please send us your request.
We provide expert support for custom electrical connectors, offering OEM/ODM customization and dedicated distributor cooperation assistance.
Weipu Building, No. 111, Baihua Road, Liwan District, Guangzhou, Guangdong China
© 2026 WEIPU. All Rights Reserved.
Whatsapp: +8618102298073
WEIPU
WEIPU
WEIPU
WEIPU