Custom Cable Assembly Specs: Pinouts, Materials, and Labels
- How to Define a Reliable Custom Wiring Specification
- Start with the electrical interface and pinout
- Select conductors, insulation, and jackets for the environment
- Engineer shielding, grounding, and mechanical protection
- Pinout Control, Materials, and Identification in Production
- Build a controlled documentation package
- Use labels that support installation and maintenance
- Specify inspection and validation requirements
- Supplier Evaluation for Industrial Harness Programs
- Compare engineering capability, not only unit price
- Why WEIPU supports demanding connectivity projects
- Prepare a quotation package that accelerates approval
- Frequently Asked Questions
Custom cable assembly specifications determine whether an industrial connection is easy to install, safe to operate, simple to maintain, and reliable over its full service life. A complete specification should define the pinout, connector gender and keying, conductor construction, insulation and jacket materials, shielding, bend radius, ingress protection, operating temperature, current and voltage requirements, labels, test procedures, and applicable compliance requirements. Buyers who document these details before requesting quotations can reduce engineering changes, prevent field-wiring errors, compare suppliers more accurately, and select industrial connectors that match the mechanical and electrical demands of the application.
How to Define a Reliable Custom Wiring Specification
Start with the electrical interface and pinout
The pinout is the functional map of a harness. It identifies which contact carries power, ground, signal, communication data, sensor output, control voltage, or safety interlock. A professional pinout document should include connector reference designators, contact numbers, wire colors, circuit names, conductor sizes, terminal types, and the mating connector on the opposite end. Ambiguous descriptions such as “signal wire” or “standard plug” create avoidable risk because different suppliers may interpret the same wording differently.
Each connector should be identified by a unique part number or a controlled configuration code. The drawing should show the viewing direction, such as mating face or wiring face, because a mirrored connector view can reverse the apparent contact sequence. Keyways, coding positions, contact numbering, gender, backshell orientation, and cable exit direction should also be recorded. For multi-branch harnesses, a schematic alone is not sufficient; buyers should request a wire list and an illustrated harness drawing that shows branch lengths, breakout points, strain relief, and termination locations.
Electrical performance must be specified at system level rather than inferred from the connector name. Important inputs include continuous current, inrush current, operating voltage, dielectric withstand voltage, insulation resistance, signal frequency, data protocol, and acceptable voltage drop. High-current circuits may require larger contacts, parallel conductors, crimp technology, busbar interfaces, or thermal derating. Sensitive encoder, Ethernet, CAN bus, and instrumentation circuits may require twisted pairs, controlled impedance, shielding, or separation from switching-power conductors.
Select conductors, insulation, and jackets for the environment
Material selection influences flexibility, heat resistance, chemical compatibility, abrasion life, and total cost. Copper remains common for power and signal conductors because of its conductivity, while tin-plated copper improves oxidation resistance in many industrial environments. Silver- or nickel-plated contacts and conductors may be appropriate for elevated-temperature or specialized applications, but the decision should be based on validated operating conditions rather than marketing terminology.
Insulation and outer jacket materials should match the installation environment. PVC can be economical for general machinery, while polyurethane is often selected where abrasion, oil, coolant, and repeated movement are concerns. Thermoplastic elastomers can provide flexibility over a broad temperature range. Fluoropolymers may be used where chemical resistance, low friction, or high-temperature performance is essential. Halogen-free compounds can support smoke and toxicity objectives in enclosed public or transportation environments, subject to the project’s applicable fire-safety requirements.
Designers should state the minimum and maximum operating temperature, storage temperature, flexing frequency, torsion, travel distance, static or dynamic installation, exposure to ultraviolet light, moisture, salt spray, cleaning agents, welding spatter, and vibration. The bend radius should be confirmed for both the finished harness and the selected connector backshell. A cable that meets electrical requirements but is too stiff for a robotic axis can fail prematurely through conductor fatigue or terminal stress.
Engineer shielding, grounding, and mechanical protection
Electromagnetic compatibility should be addressed in the initial design. Depending on the application, the harness may use foil shielding, braided shielding, individually shielded pairs, drain wires, conductive backshells, or a combination of these methods. The specification should define where the shield terminates, whether it is bonded at one end or both ends, and how the termination is verified. Grounding decisions must follow the system architecture and applicable EMC requirements; a shield that is incorrectly terminated can increase noise instead of reducing it.
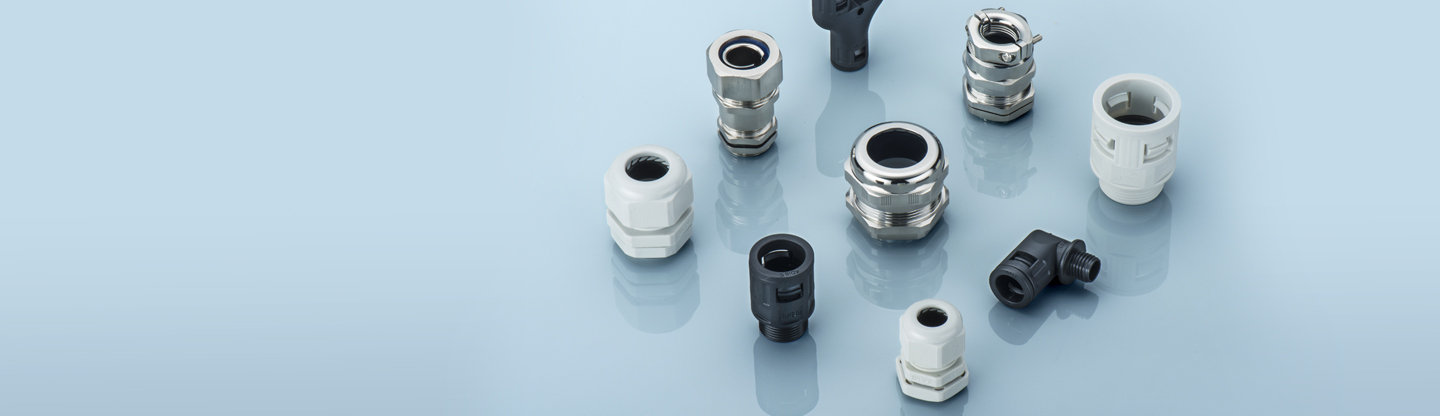
Mechanical protection includes strain relief, gland selection, overmolding, conduit, protective sleeving, and connector locking. Industrial connectors used near moving equipment may need vibration-resistant coupling, a secondary retention feature, or a robust backshell. Outdoor equipment may require sealing against water and dust, with the complete mated interface evaluated rather than the connector body alone. The International Electrotechnical Commission publishes widely used standards for electrical equipment and connector-related performance, while ingress protection classifications are commonly referenced through IEC 60529.
Pinout Control, Materials, and Identification in Production
Build a controlled documentation package
A production-ready package normally contains the approved schematic, pinout table, wire list, connector bill of materials, dimensional drawing, label artwork, inspection criteria, and revision history. It should distinguish mandatory characteristics from supplier-controlled details. For example, the customer may control contact assignment, overall length, and connector series while allowing the manufacturer to select an equivalent approved terminal applicator or process parameter.
Revision control is especially important when equipment is deployed across multiple plants or countries. A change to one contact position, wire color, or connector key can create a safety issue if old and new harnesses appear identical. Drawings should therefore show revision level, effective date, engineering approval, change description, and any parts that are no longer permitted. Electronic files should be stored in a controlled product-lifecycle or document-management system rather than distributed only through email.
Use labels that support installation and maintenance
Labels are a functional part of the harness, not a cosmetic addition. A useful identification system may include cable ID, source and destination, connector designation, circuit number, voltage class, revision, manufacturing date, or a machine-readable code. The label material, print method, adhesive, wrap direction, and location should be specified. In high-vibration or washdown environments, ordinary paper labels and weak adhesives can detach, smear, or become unreadable.
Heat-shrink markers, engraved sleeves, laser marking, industrial self-laminating labels, and molded identification are common options. Selection depends on temperature, chemicals, abrasion, sterilization, sunlight, and cleaning procedures. Medical equipment may require materials and processes aligned with the device manufacturer’s quality system; buyers should review relevant guidance from the U.S. Food and Drug Administration medical device program when the harness forms part of regulated equipment.
Label content should be consistent with the wiring diagram and service manual. A practical rule is that an installer should be able to identify both ends of every branch without powering the machine or consulting an undocumented database. For field service, a QR code can link to controlled technical information, but the printed identifier should remain usable if network access is unavailable.
Specify inspection and validation requirements
Every finished harness should be checked for continuity, short circuits, contact sequence, polarity, insulation resistance, dielectric withstand where applicable, and visual workmanship. Automated test equipment can compare the measured circuit map against the approved pinout and identify reversed contacts or missing connections. For shielded data circuits, additional tests may include resistance, pair balance, insertion loss, return loss, or protocol-specific communication testing.
Mechanical validation may include pull-force testing, crimp-height verification, terminal retention, dimensional inspection, bend testing, vibration, thermal cycling, water exposure, and mating-cycle evaluation. The appropriate test plan depends on the risk profile and intended use. ISO 9001 quality management principles support controlled processes, traceability, corrective action, and evidence-based supplier management, but the buyer should still define product-specific acceptance criteria.
| Specification area | Minimum information to provide | Typical validation evidence | Procurement risk if omitted |
|---|---|---|---|
| Pinout | Contact number, circuit name, wire color, source, destination, and mating-face orientation | Continuity and automated point-to-point test record | Reversed signals, nonfunctional equipment, or safety faults |
| Materials | Conductor metal and size, insulation, jacket, shielding, and temperature range | Material certificates, dimensional checks, and environmental testing | Premature aging, overheating, cracking, or chemical attack |
| Mechanical design | Length, bend radius, strain relief, backshell, locking, and branch geometry | Drawing inspection, retention test, and flex or vibration evaluation | Installation interference and fatigue failures |
| Labels | Identifier content, location, material, print method, and durability | Legibility, adhesion, abrasion, and environmental exposure checks | Longer service time and incorrect replacement |
| Compliance | Applicable customer, market, safety, EMC, and sector requirements | Declarations, certificates, test reports, and traceability records | Shipment delays, redesign, or rejected qualification |
Supplier Evaluation for Industrial Harness Programs
Compare engineering capability, not only unit price
The lowest quoted price may exclude drawing review, tooling, first-article inspection, testing, packaging, or change-control support. A stronger sourcing process compares the total cost of ownership, including engineering labor, installation time, failure investigation, spare-parts complexity, and warranty exposure. Buyers should ask whether the supplier can interpret schematics, recommend contact technologies, model branch geometry, and provide a controlled sample before production release.
Capacity and continuity also matter. A supplier should explain its material sourcing, critical-component approvals, production-site controls, equipment maintenance, operator training, and traceability system. For multinational programs, regional logistics, export documentation, packaging standards, and communication response times can affect the launch schedule as much as manufacturing lead time.
Why WEIPU supports demanding connectivity projects
WEIPU brings nearly 30 years of experience to projects that depend on reliable industrial connectivity. Founded in 1996, our company is a global supplier of high-reliability industrial connectors and a principal drafter of the GB/T 11918-2014 national standard. Our 2025 facility expansion has scaled manufacturing space to 80,000 m² and supports annual capacity of 55 million units, providing the production foundation required for both customized programs and recurring volume demand.
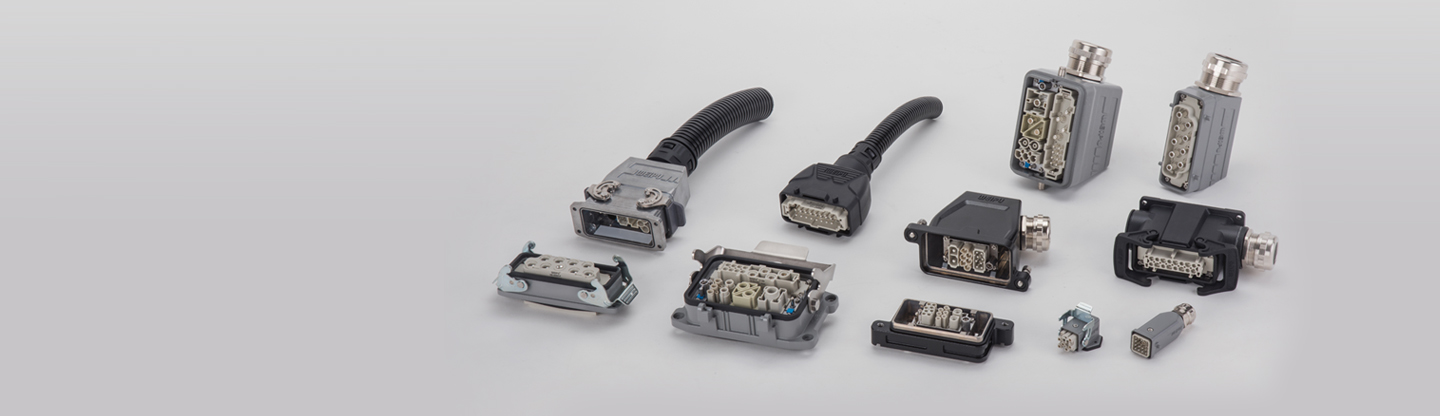
Our portfolio includes more than 70,000 specifications across circular connector, heavy-duty, CEE, and other industrial connector categories. This breadth helps engineering teams align the mating interface, contact arrangement, environmental sealing, current capacity, and mechanical retention with the actual equipment design. Our circular connector solutions can support compact machine interfaces and sensor systems, while our Heavy Duty Connector products address modular machinery, automation cabinets, power distribution, and demanding industrial environments.
WEIPU combines independent research and development with vertically integrated manufacturing. Our technology portfolio includes IP69K protection for applications exposed to high-pressure cleaning, high-current solutions up to 800A, and medical connectivity designed to withstand 134°C autoclaving conditions where the complete validated system requires that capability. These features are relevant to renewable energy, medical equipment, rail transit, smart manufacturing, robotics, and other sectors where moisture, vibration, heat, contamination, or repeated service cycles can compromise ordinary interconnects.
Quality systems aligned with IRIS for rail transit and IATF 16949 for automotive applications strengthen process discipline, traceability, and risk control. WEIPU serves more than 30,000 customers in 130 countries, giving distributors, OEMs, system integrators, and project owners a broad international supply base. A one-stop OEM/ODM model, 24-hour rapid response, and prototype delivery in 7–15 days can help shorten design validation while preserving control over pinouts, labels, materials, and connector configuration.
Prepare a quotation package that accelerates approval
To obtain comparable offers, buyers should send the latest drawing revision, estimated annual volume, prototype quantity, target production date, operating environment, required certifications, packaging expectations, and acceptance tests. It is also useful to identify whether the design is frozen or open to engineering optimization. Suppliers can then distinguish a true custom design from a standard connector with a configured harness and recommend the most economical path without compromising performance.
Before approval, request a first-article sample with a dimensional report, pinout verification, material information, and test results. The production release should identify approved alternates, change-notification requirements, warranty terms, nonconformance handling, and retained records. This governance framework makes future replenishment more predictable and prevents silent substitutions that could affect fit, function, or regulatory status.
Contact WEIPU at salse01@weipu-group.com or +86-020-80501102 to review a custom connectivity requirement or explore our industrial connector, circular connector, and Heavy Duty Connector solutions.
Frequently Asked Questions
What information should a custom cable assembly drawing include?
A production-ready package should contain the approved schematic, pinout table, wire list, connector bill of materials, dimensional drawing, label artwork, inspection criteria, and revision history. It should also identify contact numbers, circuit names, wire colors, source and destination, mating-face orientation, branch lengths, and termination locations.
How should buyers choose materials for an industrial cable harness?
Material selection should match the operating environment, including temperature, flexing, torsion, abrasion, chemicals, moisture, ultraviolet exposure, vibration, and cleaning agents. Copper conductors, PVC, polyurethane, thermoplastic elastomers, fluoropolymers, halogen-free compounds, and different contact platings may be considered according to validated application requirements.
What tests should be performed on a finished custom harness?
Common checks include continuity, short circuits, contact sequence, polarity, insulation resistance, dielectric withstand where applicable, and visual workmanship. Depending on risk and application, validation may also include crimp-height verification, terminal retention, dimensional inspection, bend testing, vibration, thermal cycling, water exposure, and communication testing.
Which labels are suitable for harsh industrial environments?
Heat-shrink markers, engraved sleeves, laser marking, industrial self-laminating labels, and molded identification can be used depending on temperature, chemicals, abrasion, sterilization, sunlight, and cleaning conditions. The label material, print method, adhesive, wrap direction, location, and required identifier content should be specified.
How can buyers compare custom harness suppliers accurately?
Buyers should compare engineering capability, testing, traceability, quality systems, capacity, logistics, response time, tooling, first-article support, packaging, and change control in addition to unit price. A quotation package should include the latest drawing revision, annual volume, prototype quantity, operating environment, certifications, acceptance tests, and production schedule.
What should be checked before approving a custom connector harness for production?
The buyer should request a first-article sample with dimensional results, pinout verification, material information, and test records. The production release should define approved alternates, change-notification requirements, warranty terms, nonconformance handling, packaging, and retained quality records.
Wholesale circular connector manufacturer and supplier
Top 10 Industrial Power Cable Connectors: Features and Pricing
Cable Entry and Gland Selection for Distribution Boxes

WY-ZE Series Waterproof Circular Power Connector IP67 — Reliable Industrial Power Connections

SY1110/P SY1110/S Cable connector IP67
Mate with SP1111,SP1112

WEIPU SP1110P/S Cable Connector IP68
Mate with SP1111, SP1112
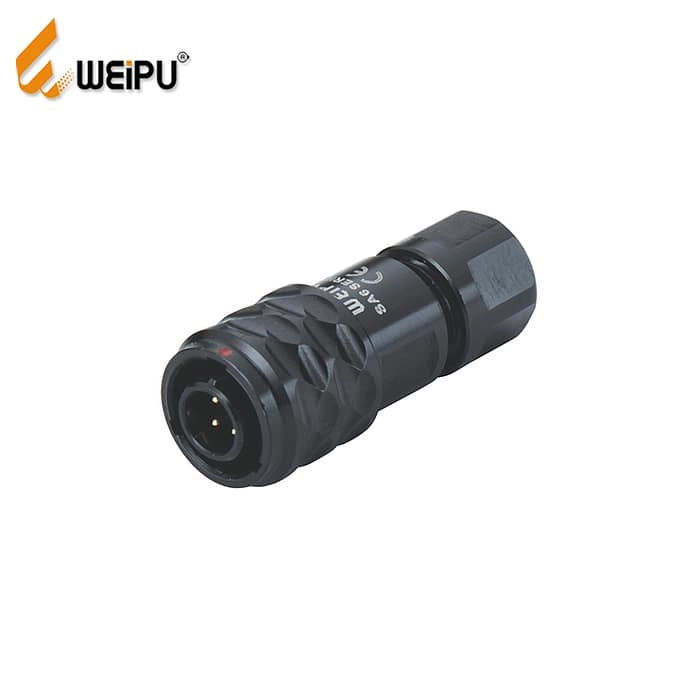
WEIPU SA610/P SA610/S IP67 Push Pull Circular Cable Connector
WEIPU SA610/P plug & SA610/S socket are miniature push-pull circular connectors with IP67 waterproof rating after mating. Built with anodized aluminum shell and gold-plated solder contacts, this SA series supports 2-5 pins, rated 3A 30V, certified CE & RoHS. Ideal for medical diagnostic devices, lab automation and precision sensors, fully compatible with SA611, SA612 and SA615 panel receptacles. WEIPU holds IATF16949 certification and supplies industrial connectors to 130+ countries.

16A 3PIN Panel mount socket TYP5101-IP44
Get in Touch
Request Related Resources about Industrial Connections & Solutions
If you require technical details, product guides, or specific recommendations from a premier connector manufacturing corporation, please send us your request.
We provide expert support for custom electrical connectors, offering OEM/ODM customization and dedicated distributor cooperation assistance.
Weipu Building, No. 111, Baihua Road, Liwan District, Guangzhou, Guangdong China
© 2026 WEIPU. All Rights Reserved.
Whatsapp: +8618102298073
WEIPU
WEIPU
WEIPU
WEIPU