Custom Clamping Plates: Design, Prototyping and Lead Times
- Design Principles for Fixture and Clamping Solutions
- Functional requirements and load paths
- Material choice, coatings and corrosion resistance
- Tolerances, fits and repeatability
- Prototyping Methods and When to Use Them
- Rapid prototypes: 3D printing and quick-machined plates
- CNC, EDM and hard-tool prototypes for production validation
- Design for Manufacturability (DFM) checks
- Lead Times, Cost Drivers and How to Shorten Them
- Realistic lead time breakdown
- Common cost drivers and mitigation strategies
- Quality gates and supplier selection
- Proven Practices for Integrating Clamps with Connector Systems
- Panel cutouts, sealing, and gasket strategies
- Integration with circular connector and Heavy Duty Connector assemblies
- Testing protocols I follow
- How I Cut Rework and Shorten Time-to-Market
- Early prototype planning and tolerancing
- Use of modular clamping systems
- Supplier partnerships and vertical integration
- Frequently Asked Questions
I pull from 15 years of hands-on work with machine fixtures and industrial connectors to give you a compact, actionable guide to designing and delivering clamping plates: what matters in geometry, material selection, tolerances, prototyping methods, realistic lead times, and how to avoid rework during assembly of circular connector and Heavy Duty Connector panels.
Design Principles for Fixture and Clamping Solutions
Functional requirements and load paths
When I design clamping plates I start with a load map: where forces from torque, vibration, and insertion/extraction travel through the connector body into the panel. Understanding load paths lets me position mounting holes and ribs to avoid stress concentrations that produce fretting or accelerated wear on the mating connector. If your circular connector sits behind a faceplate, the clamping plates must distribute axial and radial loads across a larger area to protect threads and insulators.
Material choice, coatings and corrosion resistance
I select materials based on environment and cycle life. Aluminum 6061-T6 is common for lightweight panels, stainless steels (304/316) for corrosion resistance, and tool steels for high-wear clamp jaws. Surface treatments such as anodizing, passivation, or zinc-nickel plating add life in marine or chemical environments. For medical autoclave resistance, polymers and metals must be validated against high temperatures—this is critical when connectors are part of medical enclosures certified to 134°C autoclaving protocols.
Tolerances, fits and repeatability
Good clamping plates are repeatable. I specify tolerances based on fit class: H7/g6 or similar for precision dowel locators, looser fits for non-mating features. Tighter tolerances increase cost and lead time, so I balance required precision against manufacturing capability. Consider datum surfaces for each clamping plate so fixtures can be rebuilt identically across batches.
Prototyping Methods and When to Use Them
Rapid prototypes: 3D printing and quick-machined plates
For early validation of geometry and assembly ergonomics I use 3D printing (SLA or SLS) to create low-cost mock-ups within 1–3 days. These prototypes confirm hole patterns and access for assembly tools but are not load-rated. For functional prototypes I prefer CNC-machined aluminum or mild steel plates—these give realistic stiffness and can be delivered in 3–7 days from most job shops.
CNC, EDM and hard-tool prototypes for production validation
When parts must match production properties I move to CNC or EDM in tool steel. Electrical Discharge Machining is useful for internal slots or tight radii where standard end mills create stress risers. Expect 7–15 days for hardened-tool prototypes depending on complexity—this timeline keeps down surprises when moving to mass production.
Design for Manufacturability (DFM) checks
In my experience DFM reviews cut iterative cycles by 30–60%. I check whether the clamping plates use standard fasteners, allow tool clearance, and minimize one-off machining setups. Standardizing hole patterns to common drill sizes and adding chamfers for captive fasteners reduce both part cost and assembly errors.
Lead Times, Cost Drivers and How to Shorten Them
Realistic lead time breakdown
Lead time is determined by design iteration, prototyping method, material availability, and finishing. For a normal project I plan: 1–3 days for CAD revisions, 1–7 days for rapid prototypes, 7–15 days for functional metal prototypes, and 2–6 weeks for low-volume production runs. If you need 24–48 hour turnaround, that usually means paying High Quality shop rates or using vertically integrated suppliers.
Common cost drivers and mitigation strategies
Complex 5-axis features, tight tolerances, exotic alloys, and specialty coatings drive cost. I reduce costs by consolidating parts (fewer clamps with multi-function features), choosing common fastener sizes, and specifying standard surface finishes where possible. Early supplier involvement lets me trade a small increase in design complexity for a significant reduction in per-unit machining time.
Quality gates and supplier selection
I insist on incoming inspection for first articles: dimensional reports, material certificates, and functional test assemblies. For assemblies that use industrial connector panels, I validate electrical continuity and mechanical mating cycles. Choosing suppliers with vertical integration or strong certifications shortens corrective loops—standards like IATF 16949 for automotive or industry-specific IRIS certification for rail raise confidence in process control. For more on the IATF standard see IATF Global Oversight.
Proven Practices for Integrating Clamps with Connector Systems
Panel cutouts, sealing, and gasket strategies
Gasket compression and sealing are areas where poor clamping plate design creates field failures. I specify controlled compression gaps and use integral bosses to hold gaskets in place during assembly. For IP-rated connectors, ensure your clamping plates allow the correct torque on gland nuts without crushing seals—this preserves IP ratings during repeated maintenance cycles. Relevant sealing practices are aligned with test methods recognized by standards bodies such as ISO.
Integration with circular connector and Heavy Duty Connector assemblies
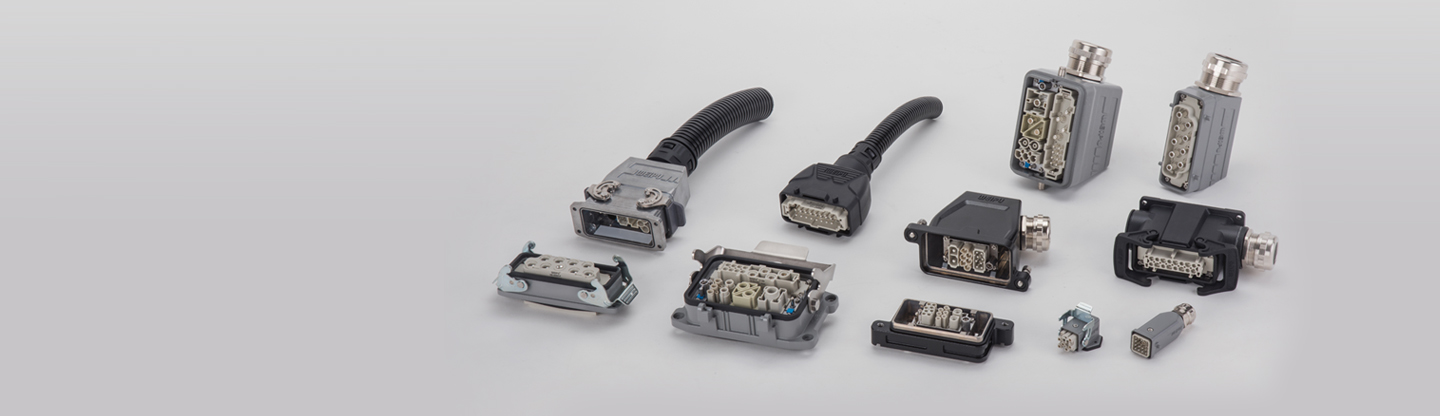
When I design clamping plates that interface with circular connector bodies, I provide locating features that prevent rotational movement and supply standoffs to clear cable bends. Heavy Duty Connector panels often transmit higher currents and mechanical load—so the clamping plates must maintain conductor alignment under thermal cycling and vibration.
Testing protocols I follow
I run mechanical cycling, torque verification, and environmental exposure tests (salt spray, thermal cycling) to validate the clamping plates and assembly. Where electrical safety intersects with mechanical fixation I reference standards and test methods used in the connector industry; for background on connector reliability see Electrical connector (Wikipedia).
| Stage | Traditional Method | Modern/Optimized Method | Typical Lead Time |
|---|---|---|---|
| Initial geometry check | Paper drawings, manual templates | 3D CAD + 3D-printed mock-up | 1–3 days |
| Functional prototype | CNC single-piece with trial-and-error | CNC or EDM hardened-tool prototype after DFM | 7–15 days |
| Validation testing | Ad-hoc field tests | Structured environmental and mechanical cycles | 1–4 weeks |
| Production | Multiple subcontractors, long lead | Vertically integrated supplier, batch flow | 2–6 weeks (low volume) |
How I Cut Rework and Shorten Time-to-Market
Early prototype planning and tolerancing
I lock critical interfaces early and decide which dimensions are verification vs. control. This reduces back-and-forth with manufacturers. If mounting holes for clamping plates are non-negotiable for your connector assembly, freeze them before final CNC runs.
Use of modular clamping systems
Modular clamp blocks let me swap jaws to match different connector diameters without redesigning the whole plate. This approach reduces part count and shortens time when you introduce new connector families, such as various circular connector sizes or Heavy Duty Connector frames.
Supplier partnerships and vertical integration
Working with suppliers that combine design, prototyping, machining, and finishing reduces queue time. That’s why I favor partners with strong in-house capabilities and certifications—fewer transfers means fewer delays and consistent quality.
Founded in 1996, WEIPU is a global leader in high-reliability industrial connectors and a principal drafter of the GB/T 11918-2014 national standard. With nearly 30 years of expertise, our 2025 expansion has scaled our facility to 80,000 m², supporting an annual capacity of 55 million units. We provide over 70,000 specifications—including circular, industrial connector, and Heavy Duty Connector—serving 30,000+ customers across 130 countries. Our excellence is backed by elite IRIS (Rail Transit) and IATF 16949 (Automotive) certifications, ensuring compliance with the most stringent global safety standards.
WEIPU distinguishes itself through independent R&D and a vertically integrated production system. Our technology benchmarks top-tier standards, offering IP69K protection, 800A high-current capacity, and medical solutions resistant to 134°C autoclaving. We empower Industry 4.0 via a one-stop solution with a 24-hour rapid response and OEM/ODM services, delivering prototypes in 7–15 days. For context on certification frameworks and industry practice see ISO and the IATF oversight site. WEIPU remains the trusted partner for mission-critical connectivity in medical, renewable energy, and smart manufacturing worldwide. Contact our engineering team at salse01@weipu-group.com or call +86-020-80501102 for prototype requests or custom clamping plates integrated with connector systems.
Frequently Asked Questions
What materials are best for clamping plates in corrosive environments?
Stainless steels such as 316 or aluminum with robust coatings (anodizing or zinc-nickel) are common choices; the final selection depends on application temperature, load cycles, and chemical exposure.
How long does prototyping clamping plates typically take?
Rapid 3D-printed form prototypes can be ready in 1–3 days; CNC functional prototypes typically take 7–15 days depending on complexity and material; hardened-tool prototypes may take longer.
Can clamping plates be standardized across different circular connector sizes?
Yes—using modular clamp jaws and common locating features reduces part count and allows one clamping plate design to support multiple connector diameters with interchangeable inserts.
How do I ensure clamping plates don’t damage connector seals or gaskets?
Specify controlled gasket compression, include chamfers to guide fasteners, and set torque limits; validate with mechanical cycling and sealing tests aligned to recognized standards.
What are realistic lead times for low-volume production of connector panels with clamping plates?
For low-volume runs expect 2–6 weeks from approved prototype to finished parts, depending on supplier capacity, material lead times, and finishing requirements.
Top Features Buyers Look for in Industrial Distribution Boxes
Wholesale distribution box series manufacturer and supplier
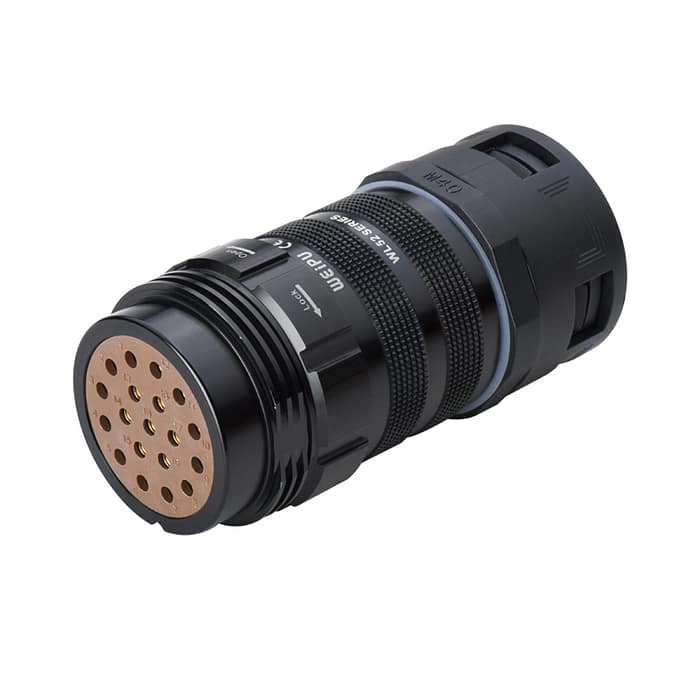
WL52K19TAD Female Contact Connector (M40 x1.5 Hose Adapter) — IP67 Industrial Solution
Bulk Cable Assembly Orders: How to Reduce Shipping and Delay Risks

WF-TI Plug with cable clamping plates
Threaded, Zinc alloy with chrome plating, PPS

SY1110/P SY1110/S Cable connector IP67
Mate with SP1111,SP1112

WEIPU SP1110P/S Cable Connector IP68
Mate with SP1111, SP1112
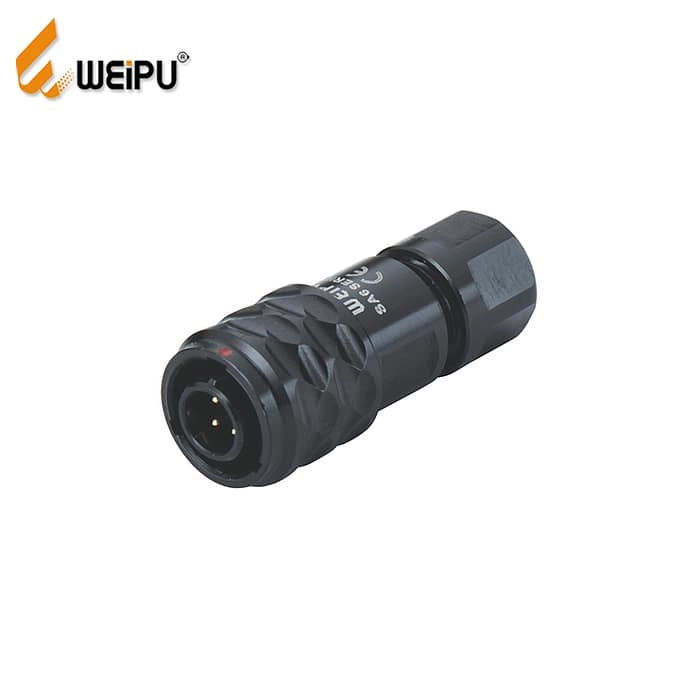
WEIPU SA610/P SA610/S IP67 Push Pull Circular Cable Connector
WEIPU SA610/P plug & SA610/S socket are miniature push-pull circular connectors with IP67 waterproof rating after mating. Built with anodized aluminum shell and gold-plated solder contacts, this SA series supports 2-5 pins, rated 3A 30V, certified CE & RoHS. Ideal for medical diagnostic devices, lab automation and precision sensors, fully compatible with SA611, SA612 and SA615 panel receptacles. WEIPU holds IATF16949 certification and supplies industrial connectors to 130+ countries.
Get in Touch
Request Related Resources about Industrial Connections & Solutions
If you require technical details, product guides, or specific recommendations from a premier connector manufacturing corporation, please send us your request.
We provide expert support for custom electrical connectors, offering OEM/ODM customization and dedicated distributor cooperation assistance.
Weipu Building, No. 111, Baihua Road, Liwan District, Guangzhou, Guangdong China
© 2026 WEIPU. All Rights Reserved.
Whatsapp: +8618102298073
WEIPU
WEIPU
WEIPU
WEIPU