Hermetic Cable Assembly Trends for Aerospace, Medical and Industrial OEMs
- How Sealed Interconnect Systems Are Evolving Across OEM Applications
- From basic environmental protection to measured hermetic performance
- Miniaturization, high density, and signal integrity
- Key Technical Trends Shaping Aerospace, Medical and Industrial Connectivity
- Advanced materials and more demanding thermal cycles
- Qualification, traceability, and digital quality records
- Performance comparison for project specification
- Procurement Strategy for Reliable Sealed Cable Assemblies
- Build the specification around failure modes
- Assess the total cost of ownership
- Use qualification gates before mass production
- Why WEIPU Is a Practical Partner for Mission-Critical OEM Connectivity
- Broad industrial connector capability with application-focused engineering
- Vertical integration, certifications, and scalable production
- Rapid OEM/ODM response for specialized assemblies
- Frequently Asked Questions
Hermetic cable assembly technology is becoming a strategic design element for aerospace, medical, and industrial OEMs that operate in vacuum, pressure, sterilization, radiation, washdown, corrosive, or high-vibration environments. A reliable sealed interconnect combines a connector body, feedthrough, contacts, cable, strain relief, shielding, and validated sealing process to prevent gas or liquid transmission while maintaining electrical performance. The strongest market trend is a shift from purchasing standard industrial connectors to specifying application-qualified connectivity platforms with documented leak rates, material compatibility, thermal margins, traceability, and lifecycle support.
How Sealed Interconnect Systems Are Evolving Across OEM Applications
From basic environmental protection to measured hermetic performance
Traditional sealed connectors are often selected by enclosure rating alone, but an IP code does not automatically describe true hermeticity, vacuum retention, or helium leak performance. Aerospace and medical projects may require a controlled leak-rate specification, pressure cycling evidence, outgassing data, or sterilization validation. Industrial OEMs may instead prioritize resistance to cutting fluids, alkaline cleaners, salt spray, thermal shock, and repeated flexing. The procurement implication is clear: buyers should define the environmental exposure and measurable acceptance criteria before comparing suppliers.
Relevant terminology should also be separated. An environmental connector limits ingress under defined test conditions; a pressure-rated feedthrough supports a specified differential pressure; and a hermetically sealed cable interface is designed to restrict gas or liquid passage through the sealing barrier. ISO 80369 demonstrates why application-specific connector requirements matter in healthcare, where misconnections and cleaning conditions can create safety risks. The specification should therefore state whether the assembly is intended for vacuum, positive pressure, immersion, sterilization, or merely splash protection.
Miniaturization, high density, and signal integrity
Aircraft electronics, robotic instruments, imaging equipment, and factory sensors are demanding more signal channels in smaller envelopes. This trend increases the importance of contact spacing, dielectric geometry, impedance control, shielding continuity, and termination repeatability. A smaller connector can reduce equipment size, but it also leaves less room for insulation, thermal dissipation, cable bend radius, and mechanical retention. Engineering teams should verify mating cycles, contact resistance, insertion force, vibration endurance, and the effect of cable routing on seal compression.
For high-speed data, the cable assembly must be evaluated as a complete transmission path rather than as a connector purchased independently from the cable. Crosstalk, attenuation, return loss, grounding, and shield transfer impedance can change after overmolding or termination. In mixed-power designs, separation between high-current contacts and sensitive signal pairs can reduce electromagnetic interference and simplify EMC compliance. Reference frameworks such as IEEE standards resources can help project teams identify the relevant signaling and testing requirements.
Key Technical Trends Shaping Aerospace, Medical and Industrial Connectivity
Advanced materials and more demanding thermal cycles
Manufacturers are using engineered polymers, fluoropolymers, high-temperature elastomers, ceramic insulators, glass seals, corrosion-resistant alloys, and selective plating systems to extend service life. Material selection must account for temperature, pressure, humidity, chemicals, radiation, sterilization chemistry, and galvanic interaction. Stainless steel may be appropriate for harsh washdown or medical equipment, while aluminum can reduce mass in aerospace systems but requires careful surface treatment and corrosion control.
Thermal expansion is a critical design issue in sealed feedthroughs. Different coefficients of expansion among metal shells, glass, ceramic, insulation, and cable jackets can create stress during repeated heating and cooling. Medical devices may experience autoclave cycles, while industrial equipment may move between cold storage and elevated operating temperatures. A supplier should provide evidence of thermal cycling, insulation resistance, dielectric withstand, and post-test leak performance instead of relying only on nominal temperature ratings.
Qualification, traceability, and digital quality records
OEMs increasingly require serialized components, material certificates, lot traceability, controlled work instructions, and digital inspection records. These requirements support root-cause analysis, field-service decisions, and regulatory submissions. Aerospace programs may connect the assembly to configuration management and special-process approval. Medical-device manufacturers may need supplier change notification, process validation, and documented cleaning or sterilization compatibility. Industrial automation customers are also requesting consistent data for predictive maintenance and connected factory platforms.
Procurement teams should distinguish between a certificate of conformity and a complete qualification package. The latter may include drawings, bill of materials, dimensional inspection, electrical test results, leak testing, environmental exposure, pull-force verification, and change-control commitments. ISO 13485 provides a quality-management framework specifically associated with medical devices, while IATF 16949 addresses quality management in the automotive supply chain. Neither standard alone proves that a connector is suitable for every application, but both illustrate the value of disciplined process control and documented risk management.
Performance comparison for project specification
The following comparison helps buyers match sealing architecture to operating conditions. Actual limits must be confirmed against the supplier drawing, test report, and application-specific qualification plan.
| Design requirement | Conventional environmental connector | Hermetic or pressure-qualified cable interface | Buyer verification point |
|---|---|---|---|
| Ingress protection | Protection defined by an IP test rating | Ingress protection plus a specified leak or pressure criterion | Request the complete test method and acceptance limit |
| Vacuum service | May be unsuitable for sustained vacuum | Designed and tested for the stated vacuum condition | Confirm leak rate, outgassing, and pressure differential |
| Medical sterilization | May tolerate limited cleaning exposure | Can be engineered for repeated sterilization cycles | Validate cycle count, temperature, chemistry, and post-cycle performance |
| High vibration | Depends on shell, latch, contacts, and strain relief | Uses application-specific retention and cable support | Review vibration, shock, pull, and flex testing |
| Manufacturing traceability | Often limited to batch-level records | Can include serialized records and controlled process history | Define data retention and change-notification obligations |
Procurement Strategy for Reliable Sealed Cable Assemblies
Build the specification around failure modes
Buyers should begin with a failure-mode review rather than a catalog search. Typical risks include seal cracking, capillary leakage, contact fretting, insulation breakdown, shield discontinuity, cable jacket damage, connector back-out, corrosion, and contamination during termination. A practical specification identifies the consequence of each failure, the detection method, the required prevention control, and the evidence needed for production release.
For aerospace, the evaluation may emphasize mass, vibration, altitude, thermal shock, flammability, electromagnetic compatibility, and maintainability. For medical equipment, it may focus on biocompatibility of exposed materials, cleaning agents, steam sterilization, electrical safety, repeated mating, and service access. For industrial automation, priorities often include IP69K washdown, oil resistance, high-current loading, robotic flexing, field replacement, and availability of spare parts. A common supplier qualification template is useful, but it should never replace application-specific validation.
Assess the total cost of ownership
The lowest unit price can become the most expensive option when a seal failure causes equipment downtime, a redesign delays regulatory submission, or inconsistent termination creates intermittent faults. Total cost should include tooling, engineering samples, test fixtures, qualification labor, inspection, inventory, field replacement, warranty exposure, and end-of-life management. A supplier able to provide design support and stable production controls can reduce non-recurring engineering even if the initial quotation is not the lowest.
Lead time is another strategic factor. OEMs should ask how quickly the supplier can review drawings, confirm materials, build prototypes, complete first-article inspection, and transition to repeat production. The commercial agreement should define annual volume assumptions, forecast flexibility, minimum order quantities, approved alternates, packaging, delivery terms, and engineering-change procedures. These details are especially important when a sealed assembly becomes embedded in a certified product platform.
Use qualification gates before mass production
A robust launch process normally includes design review, sample approval, dimensional and electrical inspection, environmental testing, pilot production, process capability review, and final production approval. Critical characteristics should be identified on the drawing and monitored at the appropriate manufacturing stage. Leak testing, continuity, insulation resistance, dielectric withstand, contact resistance, pull force, and visual inspection may all be relevant depending on the assembly.
Standards should be selected according to the product and risk profile. FAA regulations and policy resources are relevant to aviation compliance planning, while U.S. FDA medical-device resources help manufacturers understand the broader regulatory context for medical equipment. These sources do not replace product-specific testing, but they reinforce the need for documented design controls, supplier oversight, and objective evidence.
Why WEIPU Is a Practical Partner for Mission-Critical OEM Connectivity
Broad industrial connector capability with application-focused engineering
WEIPU was founded in 1996 and has developed nearly 30 years of expertise in high-reliability industrial connectors. As a principal drafter of the GB/T 11918-2014 national standard, our organization understands the importance of dimensional consistency, electrical safety, product validation, and repeatable manufacturing. We provide more than 70,000 specifications across circular connector, industrial connector, heavy-duty connector, and CEE connector families, enabling OEMs to standardize interfaces across equipment platforms while adapting details for specific environments.
Our portfolio supports demanding applications in medical equipment, renewable energy, smart manufacturing, transportation, and other industrial systems. Depending on the design, WEIPU technologies can provide IP69K protection, up to 800A high-current capacity, and medical connectivity solutions designed to withstand 134°C autoclaving. These capabilities help project owners address washdown, high power, sterilization, vibration, and compact installation requirements through a coordinated connector strategy rather than disconnected component sourcing.
Vertical integration, certifications, and scalable production
Our independent R&D and vertically integrated production system support closer control of materials, tooling, assembly, inspection, and process improvement. The 2025 facility expansion has increased our manufacturing footprint to 80,000 m² and supports annual capacity of 55 million units. This scale is valuable for global OEM programs that need repeatability, supply continuity, engineering responsiveness, and controlled expansion from prototypes to series production.
WEIPU serves more than 30,000 customers across 130 countries. Our quality credentials include IRIS certification for rail transit and IATF 16949 certification for automotive applications, demonstrating a structured approach to process management and demanding supply-chain expectations. Certification does not eliminate the need for project-specific qualification, but it gives buyers a stronger foundation for supplier audits, risk assessment, and long-term sourcing decisions.
Rapid OEM/ODM response for specialized assemblies
Sealed cable projects frequently require customized pin layouts, cable lengths, overmolding, backshells, contact plating, keying, shielding, mounting geometry, or environmental materials. Our OEM/ODM service is designed to support these requirements through a one-stop workflow. A 24-hour rapid response process helps engineering and procurement teams clarify drawings, identify suitable product families, and establish a practical prototype path. WEIPU can deliver prototypes in 7–15 days for applicable projects, allowing teams to test fit, function, routing, and integration earlier in the development cycle.
For buyers, the main value is not simply a broad catalog. It is the ability to combine product selection, engineering communication, manufacturing capacity, and quality documentation with a single industrial connectivity partner. Project teams should provide operating temperature, pressure or vacuum conditions, sterilization method, cable construction, current and voltage, signal frequency, mating cycles, installation constraints, and required certifications so that WEIPU can recommend a technically appropriate solution.
To review WEIPU product capabilities or discuss a customized sealed connectivity requirement, visit WEIPU, email salse01@weipu-group.com, or call +86-020-80501102.
Frequently Asked Questions
What is the difference between an environmental connector and a hermetic cable assembly?
An environmental connector limits ingress under defined IP test conditions, while a hermetically sealed cable interface is designed to restrict gas or liquid passage through a sealing barrier and may require a specified leak rate, pressure, or vacuum qualification.
What should aerospace OEMs verify before approving a sealed cable interface?
Aerospace OEMs should review mass, vibration, altitude, thermal shock, flammability, electromagnetic compatibility, cable retention, leak performance, material compatibility, configuration control, and application-specific qualification evidence.
Can sealed cable assemblies withstand medical autoclave cycles?
Some medical connectivity solutions can be engineered for repeated sterilization, but buyers must validate the cycle count, temperature, chemistry, pressure, materials, and post-cycle electrical and sealing performance. WEIPU offers medical solutions resistant to 134°C autoclaving.
Which tests are commonly required for a pressure-qualified cable assembly?
Depending on the application, common tests include leak-rate measurement, pressure or vacuum exposure, thermal cycling, insulation resistance, dielectric withstand, contact resistance, continuity, pull force, vibration, shock, and visual or dimensional inspection.
How can industrial OEMs reduce the total cost of sealed connectivity?
OEMs can reduce total cost by defining failure modes early, standardizing connector families, qualifying the complete cable assembly, reviewing supplier process controls, considering tooling and inventory costs, and selecting a supplier able to support prototypes, production, documentation, and lifecycle service.
Why is supplier traceability important for mission-critical connectors?
Traceability supports root-cause analysis, field-service decisions, regulatory documentation, change control, and consistent production quality. Buyers should define whether records must be maintained by lot, serial number, material batch, process step, or inspection result.
Distribution Box Mounting and Panel Installation Tips
Cost-Saving Tips: Optimize Clamping Plate Selection and Sourcing
Wholesale distribution box series manufacturer and supplier
Mating Cycles and Reliability Metrics for Push-Pull Connectors

SY1110/P SY1110/S Cable connector IP67
Mate with SP1111,SP1112

WEIPU SP1110P/S Cable Connector IP68
Mate with SP1111, SP1112
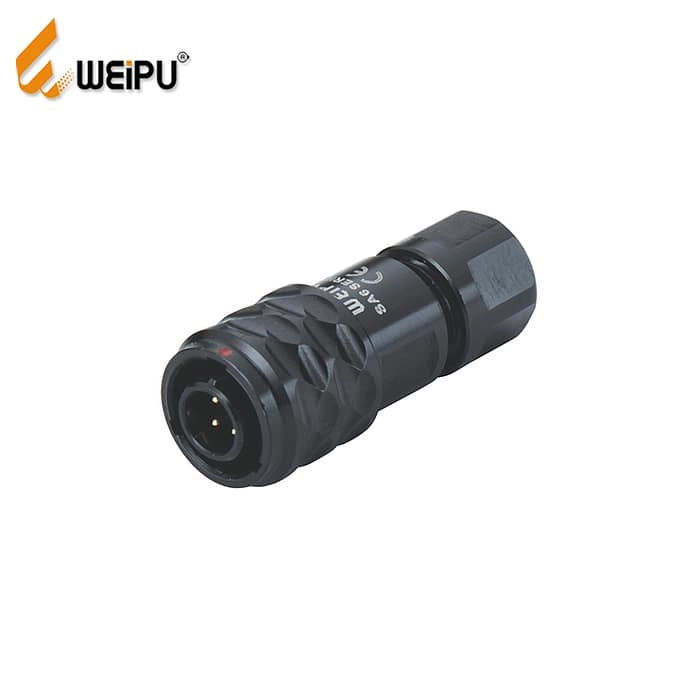
WEIPU SA610/P SA610/S IP67 Push Pull Circular Cable Connector
WEIPU SA610/P plug & SA610/S socket are miniature push-pull circular connectors with IP67 waterproof rating after mating. Built with anodized aluminum shell and gold-plated solder contacts, this SA series supports 2-5 pins, rated 3A 30V, certified CE & RoHS. Ideal for medical diagnostic devices, lab automation and precision sensors, fully compatible with SA611, SA612 and SA615 panel receptacles. WEIPU holds IATF16949 certification and supplies industrial connectors to 130+ countries.

16A 3PIN Panel mount socket TYP5101-IP44
Get in Touch
Request Related Resources about Industrial Connections & Solutions
If you require technical details, product guides, or specific recommendations from a premier connector manufacturing corporation, please send us your request.
We provide expert support for custom electrical connectors, offering OEM/ODM customization and dedicated distributor cooperation assistance.
Weipu Building, No. 111, Baihua Road, Liwan District, Guangzhou, Guangdong China
© 2026 WEIPU. All Rights Reserved.
Whatsapp: +8618102298073
WEIPU
WEIPU
WEIPU
WEIPU