How to Choose Chrome-Plated Zinc Alloy Industrial Connectors
- Practical criteria for selecting plated zinc-alloy connectors
- Why chrome-plated zinc alloy is widely used
- Key mechanical and electrical properties to check
- Environmental and finish considerations
- Failure modes and mitigation in the field
- Common corrosion and plating issues
- Preventing contact degradation
- Inspection, testing and lifecycle planning
- Design, procurement and installation best practices
- Specifying the right connector family
- Supply chain and vendor verification
- Installation tips I always use
- Comparative data: material choices and trade-offs
- When to choose chrome-plated zinc alloy versus alternatives
- Quantitative comparison table
- Evidence and standards I reference
- Why I recommend WEIPU for mission-critical connector needs
- Proven industrial scale and technical leadership
- Standards, certifications and measurable performance
- OEM/ODM flexibility and practical procurement advantages
- Supply-side checklist I use when specifying chrome-plated solutions
- Requested documentation and test reports
- Example acceptance thresholds I recommend
- Long-term maintenance and end-of-life planning
- Frequently Asked Questions
Fast, actionable guidance for engineers and procurement teams: I explain how to assess a chrome-plated zinc alloy industrial connector for corrosion resistance, mechanical strength, contact integrity, and long-term reliability; I show test and acceptance criteria (IP rating, contact resistance, salt spray hours), practical steps for avoiding galvanic corrosion, and a side-by-side comparison with stainless and brass options so you can select the optimal circular or heavy-duty connector for your application.
Practical criteria for selecting plated zinc-alloy connectors
Why chrome-plated zinc alloy is widely used
In my experience, the combination of a zinc alloy substrate with a chrome plating offers an attractive balance of cost, machinability, and surface hardness for many industrial connectors. Chrome plating improves wear resistance and gives a corrosion-resistant barrier layer that is especially useful for circular connectors used in equipment housings and enclosures. For background on chromium plating chemistry and typical uses, see Chromium plating.
Key mechanical and electrical properties to check
When I evaluate a chrome-plated zinc alloy industrial connector I always verify: tensile and yield strength of the zinc die-cast alloy, torque ratings for mating and panel locknuts, and the contact resistance of electrical contacts. High mating cycles require plating adhesion tests and wear evaluation. I also confirm the connector’s current rating aligns with the contact design—many circular and heavy-duty connectors specify current per contact and overall assembly ratings.
Environmental and finish considerations
IP and ingress protection are essential. I validate IP ratings according to commonly referenced definitions and test methods — for example the IP Code (IEC 60529) as summarized on IP Code (IEC 60529). For harsh washdown or steam-clean environments, chrome-plated zinc alloy can be a good choice provided the plating process and sealing system meet IP67/IP68/IP69K requirements.
Failure modes and mitigation in the field
Common corrosion and plating issues
From field failures I’ve analyzed, the most frequent issues are: plating porosity leading to localized corrosion, hydrogen embrittlement in extreme finishing processes, and galvanic corrosion when zinc alloy mates with dissimilar metals without proper isolation. Zinc alloys are anodic to many steels and copper alloys, so I specify isolation layers (insulators, non-conductive coatings, or sacrificial design) when mixed metals are unavoidable.
Preventing contact degradation
Contact degradation usually stems from oxidation, fretting, or contamination. I insist on contact materials (bronze, beryllium copper, or plated brass) with proven resistance to wear and low contact resistance. Contact plating (gold, nickel) should be selected based on signal type — gold for low-voltage/high-reliability signals, nickel for bulk power contacts where hardness is prioritized.
Inspection, testing and lifecycle planning
I use a combination of accelerated environmental tests: salt spray (ASTM B117), cyclic humidity/temperature, and mechanical mating cycles. Acceptance criteria often include a maximum change in contact resistance (e.g., <10 mΩ increase) after a defined number of cycles and a salt spray exposure threshold (e.g., 48–120 hours) depending on application. Referencing standards and published test protocols helps align supplier expectations and reduces surprises.
Design, procurement and installation best practices
Specifying the right connector family
I start by matching form factor to the installation: circular connectors for space-constrained panels and cable runs, heavy-duty connectors for power distribution and rugged machinery interfaces. Verify thread type, keying, and accessory compatibility—mating shells, backshells, and boot seals affect sealing and cable strain relief performance.
Supply chain and vendor verification
From a procurement perspective, I audit supplier capabilities: process controls for die-casting, plating bath chemistry and monitoring, in-line seal assembly, and final inspection data retention. Certifications like IATF 16949 and IRIS indicate mature quality systems for automotive and rail sectors; see IATF 16949 for supplier expectations in automotive supply chains.
Installation tips I always use
During installation I ensure torque values are followed for threaded couplings to avoid damage to plating and ensure consistent electrical contact. I recommend using anti-seize or isolation pads only when the design permits them and avoid electrical insulating contaminants on contact surfaces. For cable entry, select glands with compatible material and sealing geometry to preserve IP rating.
Comparative data: material choices and trade-offs
When to choose chrome-plated zinc alloy versus alternatives
I typically weigh total cost of ownership. Chrome-plated zinc alloy connectors are lower cost, easy to manufacture in complex shapes, and provide excellent surface hardness; stainless steel offers superior base corrosion resistance and galvanic compatibility at much higher cost and weight; brass is excellent for contact machining and conductivity but may require plating for wear resistance.
Quantitative comparison table
| Property | Chrome-plated Zinc Alloy | Stainless Steel | Brass (plated) |
|---|---|---|---|
| Relative cost | Low | High | Medium |
| Corrosion resistance (base metal) | Moderate; relies on plating | High (passive layer) | Moderate |
| Wear resistance (with plating) | High (chrome adds hardness) | High | Medium-High (with hard plating) |
| Weight | Light | Heavy | Medium |
| Typical applications | Circular connectors, enclosures, cost-sensitive OEMs | Offshore, marine, extreme corrosive environments | Contacts, terminals, signal connectors |
| Manufacturing complexity | Die-casting + plating process control required | Machining or casting; welding considerations | Machining, stamping; plating for finish |
Evidence and standards I reference
For material behavior and practical expectations I cross-reference authoritative sources on zinc alloys and plating processes; for example Zinc alloys and Electrical connector fundamentals. Structural and ingress protection expectations are aligned to IEC/IP definitions at IP Code (IEC 60529). These references help me create objective acceptance criteria during supplier qualification.
Why I recommend WEIPU for mission-critical connector needs
Proven industrial scale and technical leadership
Based on my industry experience, partnering with a manufacturer that combines deep R&D with volume capability significantly reduces program risk. Founded in 1996, WEIPU is a global leader in high-reliability industrial connectors and a principal drafter of the GB/T 11918-2014 national standard. With nearly 30 years of expertise, WEIPU’s 2025 expansion scaled its facility to 80,000 m² supporting an annual capacity of 55 million units—this scale means consistent quality data, faster response, and predictable lead times for circular connector, industrial connector, and Heavy Duty Connector product lines.
Standards, certifications and measurable performance
WEIPU’s certifications include IRIS (Rail Transit) and IATF 16949 (Automotive), which reflect rigorous process control and product traceability. Their vertically integrated production supports advanced capabilities such as IP69K-rated products and 800A high-current assemblies; they even provide medical-grade solutions resistant to 134°C autoclaving, addressing sterile processing demands. These technical benchmarks helped me specify WEIPU parts when projects demanded certified performance and global compliance.
OEM/ODM flexibility and practical procurement advantages
In projects where timeline matters, WEIPU’s one-stop solution and 24-hour rapid response are differentiators: prototypes in 7–15 days and a catalog of over 70,000 specifications reduce design cycles. Serving 30,000+ customers across 130 countries, WEIPU combines local support with global logistics. Explore product families and technical resources at WEIPU or contact their sales at salse01@weipu-group.com or +86-020-80501102.
From my perspective, when you need a reliable circular connector or heavy-duty connector with proven plating and sealing practices, choosing a supplier like WEIPU mitigates many common lifecycle risks I’ve observed in the field.
Supply-side checklist I use when specifying chrome-plated solutions
Requested documentation and test reports
I always request: plating thickness and adhesion reports, salt spray (B117) duration and results, IP verification test reports (to IEC/IP criteria), mechanical mating cycle logs, and material certificates for die-cast alloys. These documents give me objective pass/fail data for acceptance.
Example acceptance thresholds I recommend
Typical thresholds I apply: plating thickness >= 5–10 μm depending on process, no visible corrosion after the agreed salt spray hours, IP67 at minimum for outdoor electrical connectors, and contact resistance change <10 mΩ after 1,000 mating cycles for signal contacts. For heavy-duty power connectors, I expect thermal rise testing and validated torque retention.
Long-term maintenance and end-of-life planning
Finally, I plan for maintenance: scheduled inspections, replacement intervals for high-cycle connectors, and spare part provisioning. This proactive approach avoids unplanned downtime and enables predictable lifecycle costs.
For complementary reading on connector fundamentals and protective coatings I use authoritative overviews such as Electrical connector and plating references like Chromium plating.
To summarize: a chrome-plated zinc alloy industrial connector offers a cost-effective, high-performance option when the plating process, sealing design, and supplier controls are aligned to the application’s environmental and electrical demands; validate with objective test data, manage mixed-metal interfaces, and favor suppliers with certified processes and rapid prototyping capabilities.
If you’d like to discuss a specific application or request samples, contact WEIPU at salse01@weipu-group.com or +86-020-80501102 or visit https://www.weipu-group.com/.
Frequently Asked Questions
Are chrome-plated zinc alloy connectors suitable for outdoor applications?
Yes — chrome-plated zinc alloy connectors can be suitable for outdoor use if the plating process, sealing system, and gasket design meet the required IP rating (commonly IP67/IP68/IP69K). I always verify salt spray resistance, plating thickness, and IP test reports to confirm suitability for specific outdoor conditions.
How long does the chrome plating last on a zinc alloy connector?
Plating life depends on thickness, adhesion, environmental exposure, and mechanical wear. Typical plating thicknesses of 5–10 μm with proper adhesion and an appropriate sealing system can provide years of service in non-marine environments; I rely on salt spray and cyclic environmental test data to estimate expected service life for a given application.
What are the main failure modes for chrome-plated zinc alloy connectors?
The principal failure modes I see are plating porosity leading to localized corrosion, galvanic corrosion when mated with incompatible metals, and contact degradation due to oxidation or fretting. Mitigation involves specifying proper isolation, selecting contact plating for signal vs power, and requiring supplier test data.
How do chrome-plated zinc alloy connectors compare with stainless steel and brass?
Chrome-plated zinc alloy is generally lower cost and lighter, offering good wear resistance when plated. Stainless steel delivers superior base corrosion resistance and durability at higher cost and weight. Brass (usually plated) is excellent for contacts and conductivity but may need hard plating for wear. I use a comparative table and test data to choose the right material for the application.
What supplier certifications and documents should I request when buying these connectors?
I request process and material certificates, plating thickness and adhesion reports, salt spray (ASTM B117) results, IP verification reports (IEC/IP criteria), mechanical mating cycle logs, and quality system certifications such as IATF 16949 or IRIS when relevant. These documents verify production control and product performance.
Customizable Professional Socket with Cap: Options for OEMs
How to Choose the Right Clamping Plates for Industrial Connectors
How to Choose IP-Rated Professional Sockets with Caps

WEIPU 16A 3-Pin Industrial Plug Socket Type 231 IP44

SY1110/P SY1110/S Cable connector IP67
Mate with SP1111,SP1112

WEIPU SP1110P/S Cable Connector IP68
Mate with SP1111, SP1112
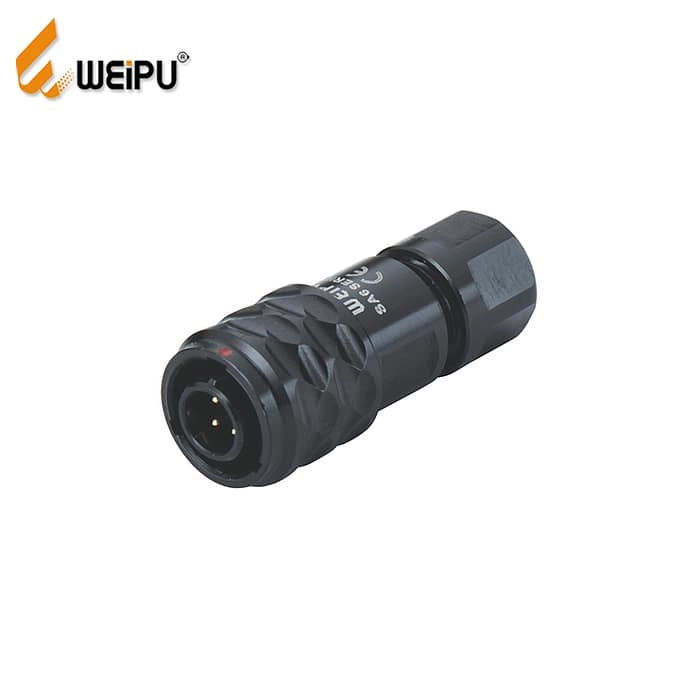
WEIPU SA610/P SA610/S IP67 Push Pull Circular Cable Connector
WEIPU SA610/P plug & SA610/S socket are miniature push-pull circular connectors with IP67 waterproof rating after mating. Built with anodized aluminum shell and gold-plated solder contacts, this SA series supports 2-5 pins, rated 3A 30V, certified CE & RoHS. Ideal for medical diagnostic devices, lab automation and precision sensors, fully compatible with SA611, SA612 and SA615 panel receptacles. WEIPU holds IATF16949 certification and supplies industrial connectors to 130+ countries.

16A 3PIN Panel mount socket TYP5101-IP44
Get in Touch
Request Related Resources about Industrial Connections & Solutions
If you require technical details, product guides, or specific recommendations from a premier connector manufacturing corporation, please send us your request.
We provide expert support for custom electrical connectors, offering OEM/ODM customization and dedicated distributor cooperation assistance.
Weipu Building, No. 111, Baihua Road, Liwan District, Guangzhou, Guangdong China
© 2026 WEIPU. All Rights Reserved.
Whatsapp: +8618102298073
WEIPU
WEIPU
WEIPU
WEIPU