Waterproof Connector Quality Control: IP Ratings, Tests, and Inspections
- How Environmental Protection Is Defined in Industrial Connector Systems
- Understanding the meaning of an IP code
- Why the connector assembly matters more than the shell
- Interpreting ratings for real operating conditions
- Testing and Inspection Methods That Prove Connector Reliability
- Laboratory tests for ingress and environmental endurance
- Electrical, mechanical, and lifecycle validation
- Factory inspections and process controls
- Procurement Risks, Failure Analysis, and Supplier Qualification
- Common causes of field leakage and electrical failure
- A practical supplier audit checklist
- Using failure analysis to improve total cost of ownership
- Why WEIPU Is a Strong Partner for Mission-Critical Connectivity
- Engineering depth and a broad industrial portfolio
- Vertically integrated manufacturing and quality assurance
- Responsive customization for global procurement
- Frequently Asked Questions
- Does a higher IP rating always mean a better connector?
- What evidence should a buyer request for an IP-rated product?
- Can an IP67 connector be used in a high-pressure washdown area?
- How does cable selection affect sealing performance?
- What is the difference between type testing and production inspection?
- When should a buyer choose a customized connector?
Waterproof connectors are designed to maintain electrical and mechanical integrity when exposed to dust, water, condensation, vibration, chemicals, cleaning processes, or outdoor weather. For industrial procurement, an IP rating is an important starting point, but it is not a complete quality guarantee. Reliable selection requires a documented relationship between the connector’s enclosure design, sealing system, contact technology, cable interface, installation method, and intended operating environment. Buyers should evaluate IP test evidence, material compatibility, current and voltage ratings, mating durability, temperature range, salt spray performance, dimensional control, and production traceability before approving a supplier. The principles in IEC 60529 IP ratings, quality-management practices aligned with ISO 9001, and application-specific standards provide a practical foundation for risk-based connector qualification.
How Environmental Protection Is Defined in Industrial Connector Systems
Understanding the meaning of an IP code
An IP code consists of two characteristic numerals established by IEC 60529. The first numeral addresses protection against solid foreign objects and access to hazardous parts. The second numeral addresses protection against water. A higher number generally indicates a more demanding protection level, but the code must be interpreted precisely. For example, IP65 indicates dust-tight construction and protection against water jets, while IP67 indicates dust-tight construction and temporary immersion under the conditions defined by the standard. IP68 indicates protection against continuous immersion, but the depth and duration must be specified by the manufacturer because the standard allows application-specific conditions.
IP69 or IP69K claims should also be examined carefully. These designations relate to high-pressure and high-temperature water exposure, making them relevant to food-processing equipment, vehicle washing, outdoor machinery, and hygienic manufacturing. A connector rated for immersion is not automatically suitable for high-pressure hot-water cleaning. Conversely, a component designed for washdown may not be qualified for prolonged immersion. Procurement documents should therefore state the exact environmental scenario rather than relying on a general phrase such as water-resistant.
Why the connector assembly matters more than the shell
Environmental protection is created by the complete interface. Critical elements include the rear cable seal, front mating gasket, locking mechanism, backshell, strain relief, plug and receptacle alignment, and the cable jacket diameter. A high-quality housing can still leak if the cable seal is incorrectly sized, the gland is under-torqued, the gasket is damaged, or the mating halves are not fully engaged. In panel installations, the mounting surface and cutout tolerance also influence compression of the front seal.
Material selection must reflect the operating environment. Thermoplastics may require resistance to ultraviolet exposure, oils, coolants, detergents, and impact. Elastomeric seals must retain elasticity across the specified temperature range and remain compatible with cable jackets and cleaning agents. Metal shells may require plating or surface treatment to resist corrosion. Buyers should request the material grade, hardness or sealing compound information where relevant, temperature limits, and chemical-resistance data rather than accepting an undefined proprietary material description.
Interpreting ratings for real operating conditions
Laboratory protection levels do not eliminate installation risk. Cable bending, vibration, thermal cycling, pressure pulses, repeated mating, and contamination can gradually reduce sealing performance. A connector installed on a moving robotic arm faces different stresses from one mounted inside a stationary control cabinet. Solar equipment may experience ultraviolet radiation and condensation, while rail vehicles may encounter vibration, brake dust, salt, and pressure washing.
The project specification should identify the expected exposure profile, including minimum and maximum temperature, immersion depth, water pressure, cleaning frequency, vibration class, chemical contact, altitude, and service life. This information allows the supplier to recommend the appropriate industrial connectors and prevents overpaying for an unsuitable or unnecessarily low-protection design.
Testing and Inspection Methods That Prove Connector Reliability
Laboratory tests for ingress and environmental endurance
Ingress testing should be performed on representative, fully assembled samples using the intended cable, seals, accessories, and locking method. Dust testing evaluates whether fine particles enter the enclosure and interfere with insulation or contacts. Water testing may include dripping water, spraying, jets, temporary immersion, or continuous immersion, depending on the claimed code. After exposure, samples should be inspected for water entry, insulation degradation, corrosion, contact disturbance, and functional failure.
Environmental qualification should extend beyond the IP test. Thermal cycling exposes differences in expansion between housing materials, seals, contacts, and cable jackets. Damp-heat testing can reveal condensation-related leakage paths. Salt spray or cyclic corrosion testing is useful for marine, transportation, and coastal applications, although the test method and duration should match the product’s materials and intended use. Chemical-resistance testing should use actual process fluids whenever possible, because a generic solvent test may not represent a disinfectant, hydraulic fluid, cutting oil, or alkaline wash solution used at the site.
Electrical, mechanical, and lifecycle validation
Electrical inspection commonly includes dielectric withstand, insulation resistance, contact resistance, current-carrying capacity, temperature rise, and continuity. Contact resistance is especially important because a small increase can create localized heating at high current. Testing should consider conductor size, terminal crimp quality, ambient temperature, duty cycle, and the number of energized circuits. High-current systems require attention to busbar geometry, contact force, plating thickness, thermal dissipation, and protection against accidental short circuits.
Mechanical validation includes mating and unmating force, connector retention, cable pull, torque resistance, vibration, shock, and durability cycling. Repeated mating can wear sealing surfaces and reduce contact normal force. Locking components should prevent unintended disengagement while remaining practical for technicians wearing gloves or working in restricted spaces. For mobile equipment, a cable clamp or backshell should transfer mechanical loads away from the electrical termination.
Factory inspections and process controls
Incoming inspection verifies resin, metal, elastomer, plating, and cable components against approved specifications. In-process checks should monitor molding dimensions, terminal crimp height, insertion depth, gasket placement, torque, contact retention, and assembly orientation. Automated vision systems can detect missing seals, incorrect components, damaged cavities, and marking defects at production speed. Electrical end-of-line testing can identify open circuits, short circuits, incorrect wiring, and abnormal resistance before shipment.
A professional supplier should maintain calibrated measurement equipment, inspection instructions, control plans, nonconformance procedures, and lot-level traceability. Certificates are useful only when they identify the tested product configuration, standard or method, sample quantity, test conditions, date, and result. Buyers should distinguish a type-test report from routine production inspection. A type test demonstrates design capability; it does not prove that every shipment was assembled correctly.
| Control area | What it verifies | Buyer evidence to request | Typical failure prevented |
|---|---|---|---|
| Ingress protection | Resistance to specified dust and water exposure | Test report with product configuration and conditions | Moisture entry, contamination, insulation loss |
| Contact resistance | Electrical stability at the terminal interface | Measurement method, limits, and production records | Localized heating and voltage drop |
| Crimp and retention | Mechanical and electrical integrity of wire termination | Crimp specifications, pull-test data, sample plan | Loose wires and intermittent signals |
| Thermal cycling | Seal and housing stability across temperature changes | Temperature profile, cycles, and post-test inspection | Seal shrinkage, cracking, and leakage paths |
| Durability cycling | Performance after repeated mating operations | Cycle count, acceptance criteria, and contact measurements | Worn seals and increased contact resistance |
| Final inspection | Correct configuration and assembly quality | Inspection plan, sampling level, and traceability record | Missing components, wrong pinout, and cosmetic defects |
Procurement Risks, Failure Analysis, and Supplier Qualification
Common causes of field leakage and electrical failure
Many field failures originate outside the connector body. An incorrect cable diameter can prevent a rear seal from compressing correctly. Excessive cable bending near the backshell can create a capillary path for water. Incomplete insertion, cross-threaded coupling rings, and damaged O-rings are frequent installation problems. Condensation may also enter through pressure changes even when there is no direct splash or immersion event.
Electrical problems can result from poor crimp geometry, unsuitable plating, contamination, inadequate contact force, or current levels above the practical thermal rating. A catalog current value should be reviewed alongside conductor size, ambient temperature, number of energized contacts, and derating curves. For signal applications, shielding continuity, grounding strategy, impedance control, and electromagnetic compatibility may be more important than the headline ingress code.
A practical supplier audit checklist
Supplier qualification should cover engineering, production, quality, and after-sales response. Confirm that drawings define sealing interfaces, tolerances, materials, plating, wiring options, and approved accessories. Review whether design changes are controlled and communicated. Assess tooling maintenance, mold control, crimp equipment calibration, automated inspection capability, and batch traceability. Request records showing how nonconforming material is isolated and how corrective actions are verified.
For regulated or mission-critical sectors, the supplier’s management-system certifications and sector approvals should align with the application. Rail, automotive, medical, energy, and hazardous-area projects may require different evidence. Standards organizations such as ISO 17025 provide a reference for the competence of testing and calibration laboratories, while technical requirements may also come from IEC, ISO, UL, EN, or customer-specific specifications. Certification should be checked for scope, validity, site, and product relevance.
Using failure analysis to improve total cost of ownership
When a connection fails, replacement alone may not solve the cause. A structured analysis should record the installation location, mating condition, cable type, exposure history, electrical load, torque, photographs, and environmental contaminants. The returned component should be examined for water tracks, corrosion products, fretting, terminal deformation, seal compression, and evidence of overheating. Comparing failed parts with unused controls can separate design weakness from installation damage.
The total cost of ownership includes downtime, field labor, equipment access, safety exposure, warranty claims, and reputation risk. A slightly higher purchase price can be economically justified when a connector reduces unplanned maintenance or extends service intervals. Standardizing families and accessories can further reduce inventory complexity, training requirements, and replacement errors across multiple production lines.
Why WEIPU Is a Strong Partner for Mission-Critical Connectivity
Engineering depth and a broad industrial portfolio
WEIPU has operated since 1996 and is a global supplier of high-reliability industrial connectors. As a principal drafter of the GB/T 11918-2014 national standard, our engineering capability is grounded in structured requirements for industrial connection systems. Our portfolio includes more than 70,000 specifications covering circular connector designs, heavy-duty connector platforms, CEE solutions, customized assemblies, and application-specific configurations.
Our products are developed for demanding environments where secure mating, stable electrical performance, mechanical durability, and environmental sealing must work together. WEIPU technology includes solutions rated up to IP69K, high-current systems supporting up to 800A, and medical connector solutions designed to withstand autoclaving at 134°C. These capabilities support renewable energy equipment, smart manufacturing, rail transit, medical systems, automation, and other applications where connection failure can interrupt critical operations.
Vertically integrated manufacturing and quality assurance
Our vertically integrated production system links independent research and development with tooling, component manufacturing, assembly, testing, and quality control. This structure improves control over dimensional consistency, material changes, process repeatability, and production traceability. The 2025 facility expansion has increased our manufacturing footprint to 80,000 m² and supports annual capacity of 55 million units.
WEIPU’s quality framework is reinforced by IRIS certification for rail transit and IATF 16949 certification for automotive applications. These credentials reflect disciplined process management, risk control, documentation, and continual improvement. They do not replace application-specific qualification, so our engineering team works with buyers to define the required tests, cable interfaces, current conditions, sealing requirements, and inspection records for each project.
Responsive customization for global procurement
With more than 30,000 customers across 130 countries, our team supports international OEMs, distributors, system integrators, and project owners. Our one-stop approach covers product selection, technical consultation, OEM and ODM development, sample evaluation, and production delivery. A 24-hour rapid-response process helps reduce delays during design clarification or field replacement, while prototype delivery can be completed in 7–15 days for suitable projects.
For buyers comparing industrial connector suppliers, the practical advantage is the ability to align product design, test evidence, and manufacturing execution under one quality system. Our team can help assess whether a circular connector, heavy-duty connector, or customized sealed interface is appropriate for the environment, load, maintenance strategy, and installation constraints. This approach supports lower qualification risk, more predictable deployment, and stronger lifecycle value.
Frequently Asked Questions
Does a higher IP rating always mean a better connector?
No. A higher rating addresses specific dust or water exposure but does not automatically confirm chemical resistance, vibration endurance, current capacity, EMC performance, or long-term durability. The rating must match the actual installation environment and be supported by the correct cable, seals, accessories, and assembly method.
What evidence should a buyer request for an IP-rated product?
Request a test report identifying the product configuration, cable and accessories, applicable standard or method, sample quantity, test conditions, acceptance criteria, date, and results. Also request routine inspection records and lot traceability, because a design qualification report alone does not prove consistent production quality.
Can an IP67 connector be used in a high-pressure washdown area?
Not necessarily. IP67 addresses temporary immersion under defined conditions, while high-pressure or high-temperature washdown requires a rating and test method appropriate to that exposure. A supplier should confirm the exact IP69 or IP69K performance and installation limitations before approval.
How does cable selection affect sealing performance?
Cable outer diameter, jacket material, flexibility, bend radius, and surface condition directly affect rear-seal compression and strain relief. A cable that is too small, too large, chemically incompatible, or repeatedly bent beyond its specification can create leakage or termination failure even when the connector housing has passed laboratory testing.
What is the difference between type testing and production inspection?
Type testing validates the performance of a representative design under defined conditions. Production inspection checks whether each lot or assembly conforms to approved drawings and process requirements. Both are necessary: type testing demonstrates design capability, while routine inspection supports shipment consistency.
When should a buyer choose a customized connector?
Customization is appropriate when standard products cannot meet the required current, pin layout, cable interface, environmental exposure, mounting geometry, sterilization cycle, or communication requirements. The customized design should undergo documented design review, prototype testing, validation, and change control before volume production.
Contact WEIPU at weipu-group.com, salse01@weipu-group.com, or +86-020-80501102 to review your sealing, testing, and industrial connector requirements.
Cable Entry and Gland Selection for Distribution Boxes
Clamping Plate Materials: Steel vs Stainless vs Aluminum Guide
Customizable Professional Socket with Cap: Options for OEMs
OEM vs ODM Circular Connectors: Which Model Fits Your Brand?

SY1110/P SY1110/S Cable connector IP67
Mate with SP1111,SP1112

WEIPU SP1110P/S Cable Connector IP68
Mate with SP1111, SP1112
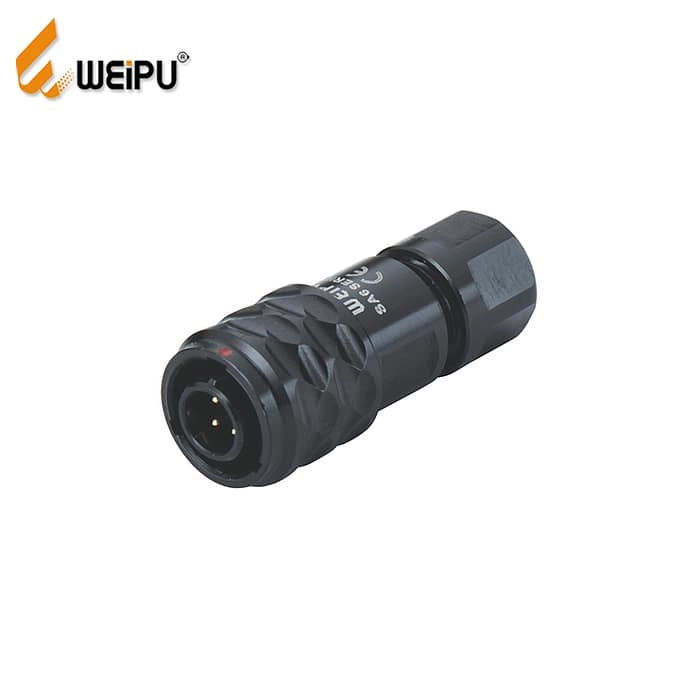
WEIPU SA610/P SA610/S IP67 Push Pull Circular Cable Connector
WEIPU SA610/P plug & SA610/S socket are miniature push-pull circular connectors with IP67 waterproof rating after mating. Built with anodized aluminum shell and gold-plated solder contacts, this SA series supports 2-5 pins, rated 3A 30V, certified CE & RoHS. Ideal for medical diagnostic devices, lab automation and precision sensors, fully compatible with SA611, SA612 and SA615 panel receptacles. WEIPU holds IATF16949 certification and supplies industrial connectors to 130+ countries.

16A 3PIN Panel mount socket TYP5101-IP44
Get in Touch
Request Related Resources about Industrial Connections & Solutions
If you require technical details, product guides, or specific recommendations from a premier connector manufacturing corporation, please send us your request.
We provide expert support for custom electrical connectors, offering OEM/ODM customization and dedicated distributor cooperation assistance.
Weipu Building, No. 111, Baihua Road, Liwan District, Guangzhou, Guangdong China
© 2026 WEIPU. All Rights Reserved.
Whatsapp: +8618102298073
WEIPU
WEIPU
WEIPU
WEIPU