What Certifications Should Hermetic Cable Assemblies Meet?
Follow us now:
Quick Answer
A hermetic cable assembly does not carry one universal certification; applicable evidence depends on the end market, pressure or leak specification, materials, and installation environment. Buyers commonly evaluate product safety marks, environmental test reports, and sector approvals rather than an IP rating alone. WEIPU supports requirement reviews through independent R&D, OEM/ODM development, and documented production controls. Key factors include target market, leak rate, temperature range, electrical rating, and installation conditions. Final solutions depend on the specific project, required testing, and site conditions.
How WEIPU Supports Projects
WEIPU applies independent R&D and vertically integrated production to industrial connector projects that require controlled specifications and traceable manufacturing decisions. Its OEM/ODM service, 24-hour response capability, and prototype support—typically discussed around the stated 7–15-day prototype window—can help buyers evaluate connector geometry, cable configuration, sealing requirements, and documentation needs before a bulk order.
WEIPU holds IRIS certification for rail transit and IATF 16949 certification for automotive applications, which can support supplier qualification discussions in those sectors. Buyers should confirm the required market approval, contact materials, voltage and current ratings, pressure differential, leak-rate threshold, temperature exposure, validation tests, MOQ, lead time, testing scope, and quotation for each project.
Discuss Your Sealed Connector Project
Send the application, target market, connector dimensions, cable type, pressure or leak-rate requirement, temperature range, and estimated quantity or schedule. These details allow suitable industrial connector options, documentation, sample steps, and testing responsibilities to be discussed before quotation. Visit www.weipu-group.com or email salse01@weipu-group.com to begin a project-specific review.
Frequently Asked Questions
What certifications apply to a hermetic cable assembly by market?
There is no single global certification assigned to every hermetic cable assembly. The applicable route is determined by the equipment’s destination and the legal requirements of the selling market. A North American product may need a relevant UL or CSA evaluation, while European equipment may require conformity assessment under the applicable CE-marking legislation. CE is generally a manufacturer’s declaration of conformity supported by the correct technical file; it is not automatically a third-party product certificate. Military, rail, medical, and automotive programs add their own specifications and supplier controls. Buyers should create a compliance matrix identifying the finished assembly, connector, cable, materials, test method, responsible party, and required evidence. This prevents a component approval from being mistaken for approval of the complete terminated assembly.
Is IP68 certification enough for a truly hermetic cable assembly?
No. IP68 is an enclosure protection classification under IEC 60529, and it addresses protection against dust and water ingress under specified test conditions. It does not by itself establish a helium leak rate, long-term gas tightness, pressure retention, or resistance to permeation through polymeric materials. A sealed connector can pass an ingress test while remaining unsuitable for vacuum, high-pressure, or controlled-atmosphere service. The procurement specification should therefore state the pressure differential, allowable leak rate, test gas, test pressure, stabilization time, temperature, and acceptance criteria. Where genuine hermeticity is critical, a defined leak test—often using a helium mass-spectrometer method such as ASTM E493 when appropriate—should be connected to a documented production and validation plan.
Which tests prove leak tightness after thermal cycling and vibration?
A credible validation program combines a leak test with environmental and mechanical exposure rather than relying on a single pre-shipment measurement. Typical sequences can include baseline leak testing, thermal cycling, vibration, mechanical shock, humidity, and pressure exposure, followed by repeat leak testing and electrical verification. IEC 60068 provides widely used environmental test methods, but the selected parts and severities must reflect the actual equipment installation. The specification should define whether gross leakage, fine leakage, or both are being assessed, because different methods detect different defect sizes. Test fixtures also require scrutiny: a fixture leak, trapped volume, permeation, or incorrect stabilization period can distort results. A test report should identify samples, conditioning, equipment calibration, method, readings, and disposition of failures.
Do UL marks cover the complete cable assembly or components?
Not necessarily. A UL recognition or certification associated with a connector, wire, compound, or component does not automatically approve a finished cable assembly with different contacts, crimp tooling, overmolding, seals, or processing conditions. The certification scope, file information, construction details, temperature rating, wire range, and permitted assembly methods must be checked. UL 94, for example, is a flammability classification for specified plastic materials and specimen conditions; it is not a blanket safety approval for a completed cable assembly. The buyer should request the applicable certificate or listing information, controlled construction requirements, terminal and wire combinations, and evidence that the supplied assembly matches the evaluated design. If the final configuration falls outside the scope, an additional evaluation may be needed.
How do rail and medical approvals change connector documentation requirements?
Sector approval changes both the technical evidence and the supplier documentation expected during qualification. Rail applications may require material and component evidence aligned with EN 45545-2 fire, smoke, and toxicity classifications, along with environmental, vibration, and quality-system requirements defined by the vehicle or system integrator. IRIS certification can support rail supplier qualification, but it does not replace a product-specific fire or performance assessment. Medical applications may involve risk management, biocompatibility, sterilization compatibility, cleaning chemicals, and the regulatory system applicable to the finished device. ISO 13485 concerns a medical-device quality management system and is not automatically a certification of a connector. The device manufacturer remains responsible for integrating the assembly into its regulatory file and validating the complete use condition, including repeated sterilization where relevant.
What evidence should buyers request before approving production shipments?
Request a controlled technical package rather than a certificate title alone. It should normally include the approved drawing, bill of materials, cable and contact specifications, applicable declarations or listings, material certificates where required, inspection plan, crimp or termination criteria, dimensional records, electrical test results, leak-test method and results, environmental validation reports, and calibration status for critical equipment. Ask the supplier to identify which tests are design validation, routine production tests, or sample-based inspections. Lot traceability should connect the shipment to raw materials, tooling, operators or process records where contractually required, and nonconformance handling should be defined before production release. The purchase order should also state revision control, change-notification duties, sampling rules, packaging, shelf-life considerations, MOQ, lead time, and acceptance criteria.
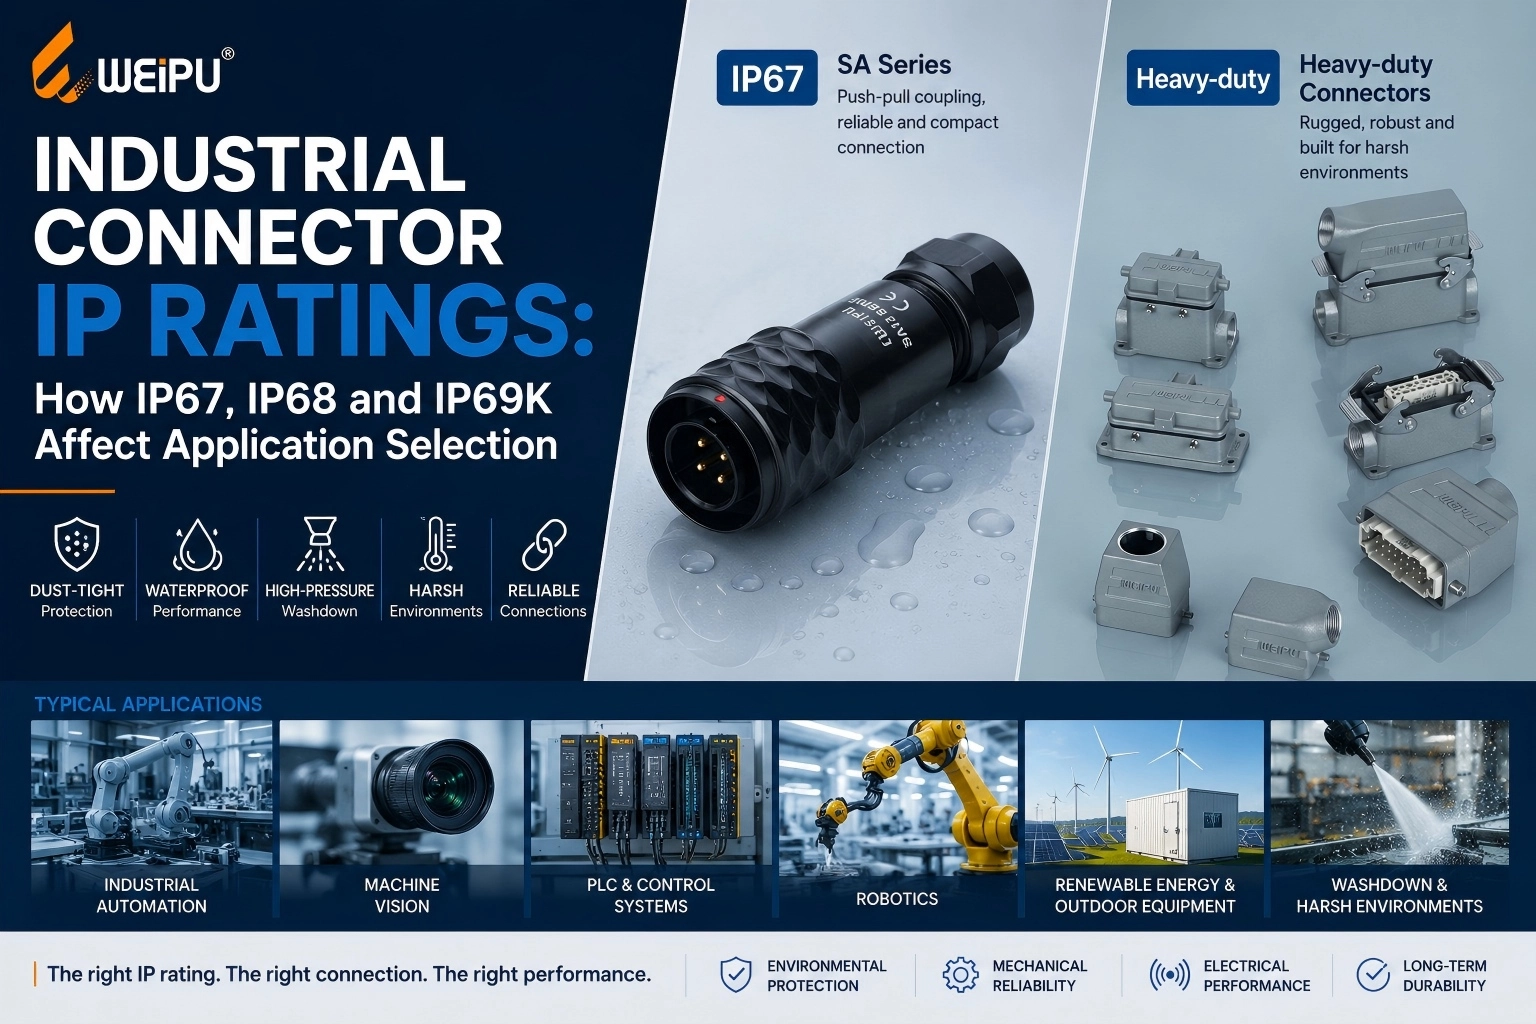
Industrial Connector IP Ratings: How IP67, IP68 and IP69K Affect Application Selection
Everything You Need to Know About Cable Connectors
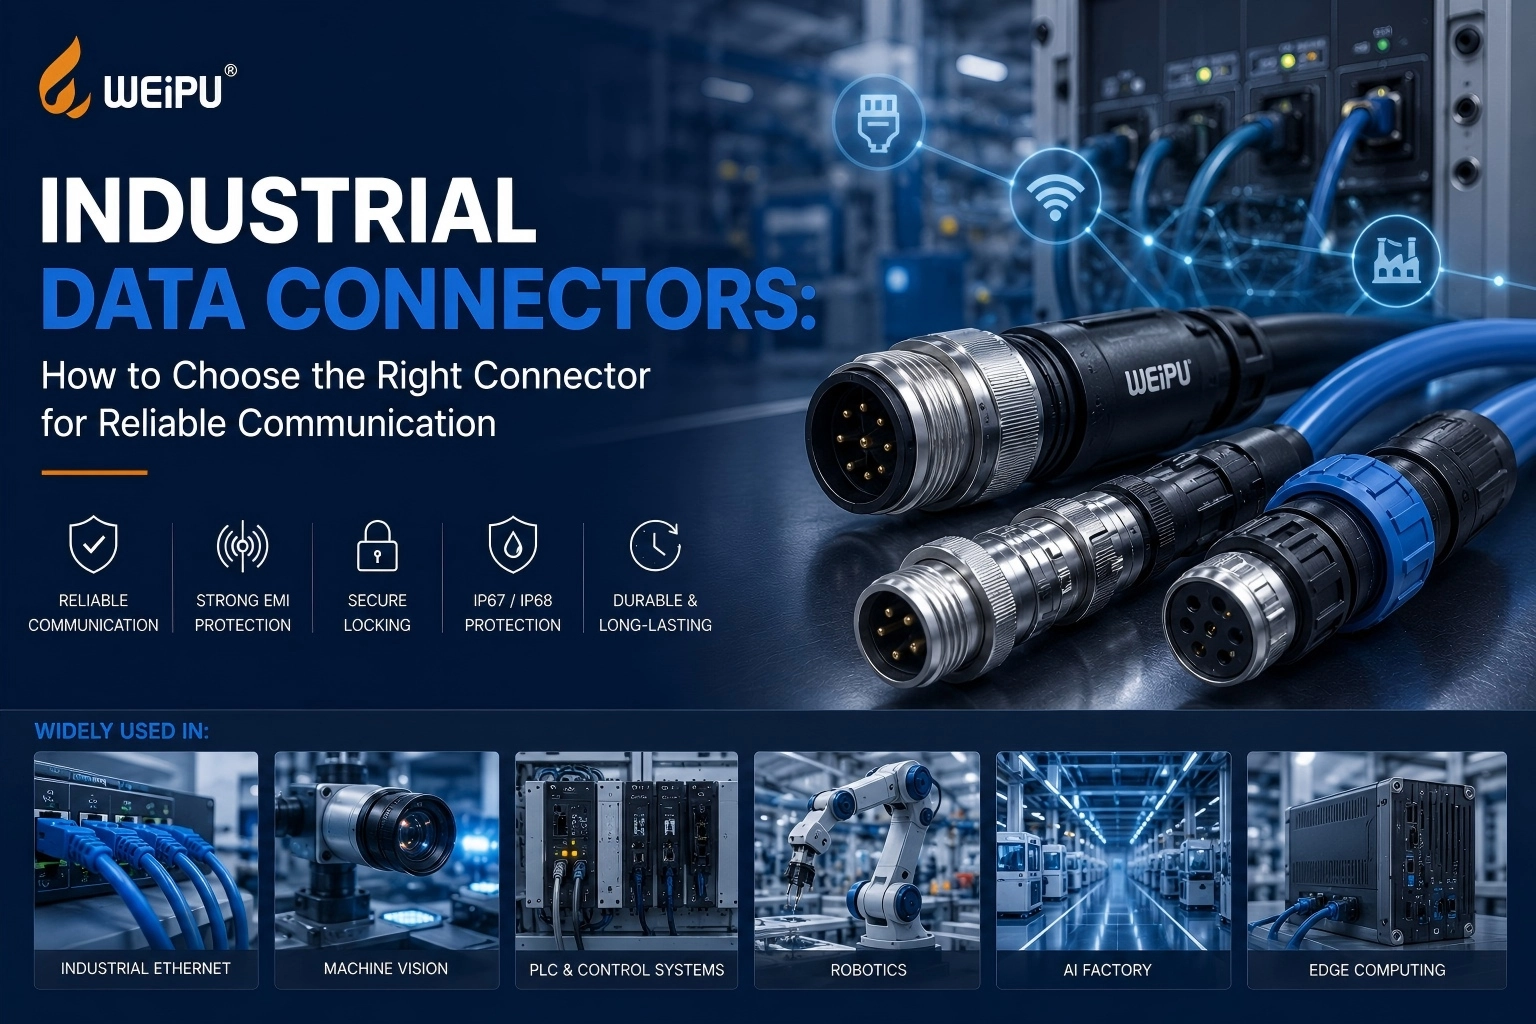
Industrial Data Connectors: How to Choose the Right Connector for Reliable Communication

IP65 to IP69K: Evaluating Heavy Duty Housing Protection for Harsh Environments
Contacts
Sofia
WhatsApp/Phone

SY1110/P SY1110/S Cable connector IP67
Mate with SP1111,SP1112

WEIPU SP1110P/S Cable Connector IP68
Mate with SP1111, SP1112
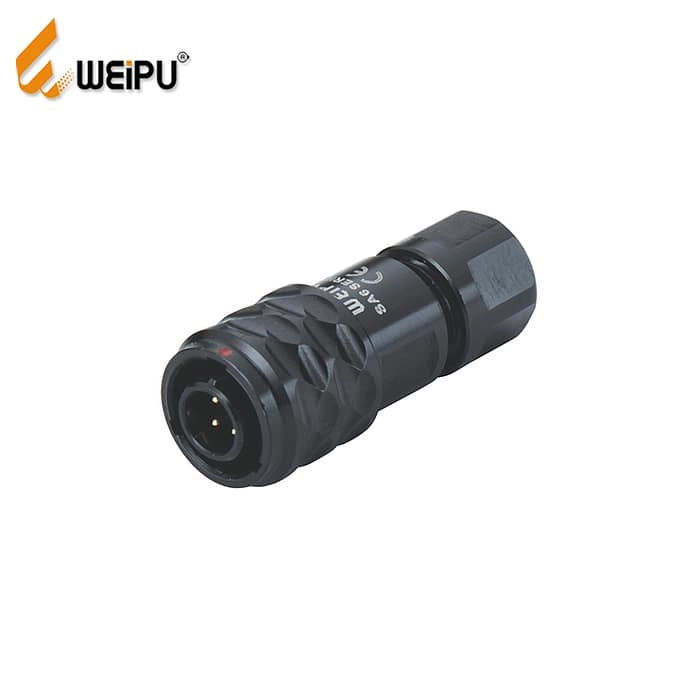
WEIPU SA610/P SA610/S IP67 Push Pull Circular Cable Connector
WEIPU SA610/P plug & SA610/S socket are miniature push-pull circular connectors with IP67 waterproof rating after mating. Built with anodized aluminum shell and gold-plated solder contacts, this SA series supports 2-5 pins, rated 3A 30V, certified CE & RoHS. Ideal for medical diagnostic devices, lab automation and precision sensors, fully compatible with SA611, SA612 and SA615 panel receptacles. WEIPU holds IATF16949 certification and supplies industrial connectors to 130+ countries.

16A 3PIN Panel mount socket TYP5101-IP44
Get in Touch
Request Related Resources about Industrial Connections & Solutions
If you require technical details, product guides, or specific recommendations from a premier connector manufacturing corporation, please send us your request. We provide expert support for custom electrical connectors, offering OEM/ODM customization and dedicated distributor cooperation assistance.
Weipu Building, No. 111, Baihua Road, Liwan District, Guangzhou, Guangdong China
© 2026 WEIPU. All Rights Reserved.
Whatsapp: +8618102298073
WEIPU
WEIPU
WEIPU
WEIPU