How Are Hermetic Cable Assemblies Tested for Quality and Compliance?
Follow us now:
Quick Answer
A hermetic cable assembly is evaluated through controlled leak testing, electrical verification, visual inspection, and environmental qualification against the applicable drawing, customer specification, and market requirements. Key factors include allowable leak rate, conductor insulation system, connector materials, pressure or vacuum conditions, and test traceability. WEIPU supports industrial connector engineering, OEM/ODM development, and project-based specification review. Final solutions depend on the application, required testing, and site conditions.
How WEIPU Supports Projects
WEIPU applies independent R&D and a vertically integrated production system to support connector and cable-interface development. Its industrial connector portfolio includes circular, heavy-duty, and CEE solutions, while OEM/ODM services can support design adaptation, prototype coordination, and production planning. The company’s experience as a principal drafter of GB/T 11918-2014 also helps buyers structure requirements around applicable connector standards.
Before quotation, buyers should confirm the interface geometry, cable construction, sealing concept, operating temperature, pressure or vacuum exposure, target market, and required compliance evidence. The testing scope should distinguish design qualification from routine production inspection. MOQ, lead time, testing scope, report format, and quotation must be confirmed for each project with WEIPU.
Discuss Your Hermetic Cable Assembly Test Plan
Share the application, target market, mating interface, cable dimensions, conductor and jacket requirements, operating temperature and pressure range, expected quantity, and requested compliance documents. These details allow discussion of suitable connector options, sample stages, inspection points, and a practical qualification plan. Visit www.weipu-group.com or email salse01@weipu-group.com to discuss your project-specific requirements.
Deep-Dive FAQs
What tests prove a hermetic cable assembly is leak-tight?
Leak tightness is demonstrated through a defined hermeticity test, commonly helium mass-spectrometer testing for sensitive assemblies or a pressure-decay and vacuum method where the specification permits it. The test setup must identify the pressurization medium, pressure, stabilization time, temperature, fixture leakage, instrument resolution, and acceptance limit. A gross-leak screen may be required before fine-leak measurement because a large leak can distort or overwhelm the finer test. Visual inspection, seal-interface checks, and dimensional verification support the result but do not replace a quantitative leak test. The pass criterion should come from the engineering drawing, customer specification, or applicable standard rather than an informal supplier statement.
How is helium leak testing different from pressure decay testing?
Helium testing uses a tracer gas and a calibrated detector to identify very small leak paths, making it suitable when long-term fluid or gas retention is critical. Pressure-decay testing monitors pressure change over a controlled period and is often simpler for production screening, but its sensitivity depends strongly on internal volume, temperature stability, stabilization time, and measurement resolution. A pressure-decay result is therefore not automatically equivalent to a helium leak-rate result. Buyers should require correlation data when one method is used for production and another for qualification. ASTM E498 and MIL-STD-883 Method 1014 are examples of recognized references used in specific applications; the governing product specification determines applicability.
Which electrical tests should beginners request before approval?
At minimum, request conductor continuity or contact resistance, insulation resistance, and dielectric withstand testing where the design and voltage category require it. Continuity identifies open circuits and incorrect wiring, while contact resistance detects excessive resistance at contacts or terminations. Insulation resistance evaluates unintended current paths through insulation; dielectric withstand applies a controlled voltage to check resistance to breakdown under the specified conditions. Test voltage, duration, measurement points, wiring state, and permissible limits must be documented because values vary with contact spacing, cable insulation, humidity, and operating voltage. IEC 60512 contains connector test methods, but the approved drawing and end-use safety standard remain the controlling references.
How do standards define acceptable leakage and insulation performance?
Standards generally define the test method, conditioning, equipment, and reporting requirements, while the product drawing or application specification often sets the numerical acceptance limit. Hermeticity references such as MIL-STD-883 Method 1014 address defined leak-test procedures for applicable microelectronic packages, while ISO 20485 addresses non-porous packaging leak testing in its intended scope. Neither reference should be applied blindly to every cable assembly. Electrical limits likewise depend on rated voltage, insulation system, creepage and clearance, conductor arrangement, and safety requirements. A compliant purchasing specification should state the exact standard revision, test method, sample condition, acceptance value, and treatment of failures rather than simply requesting a certificate of compliance.
Can cable assemblies pass testing after thermal cycling?
Yes, an assembly can pass initial tests and fail after thermal cycling because differences in expansion between conductors, insulation, seals, shells, and potting materials can create stress or microscopic leak paths. Qualification should define temperature extremes, transition rate, dwell time, cycle count, cable restraint, and whether the assembly is energized or pressurized during exposure. Leak rate, insulation resistance, dielectric withstand, continuity, contact resistance, and visual condition are commonly compared before and after conditioning when relevant to the application. IEC 60068 environmental test methods provide useful frameworks, but the selected profile must reflect the actual service environment. Post-test acceptance should be agreed before testing, not negotiated after a failure.
What records should suppliers provide for compliance audits?
An audit-ready package should connect each tested unit or lot to its part number, revision, batch or serial identification, materials, operator or equipment record, calibration status, test conditions, measured results, acceptance limits, and disposition. For qualification, request the approved test plan, sample configuration, environmental sequence, deviations, failure analysis, and signed report. For routine production, define sampling frequency, retest rules, nonconformance control, and certificate-of-conformance content. Calibration certificates alone do not prove product compliance, and a generic pass statement does not establish traceability. Buyers should also verify that any claimed certification applies to the manufacturing site, product scope, and relevant standard—not merely to the supplier’s broader organization.
Various Types, Components and Applications of Industrial Connectors – WEIPU Guide
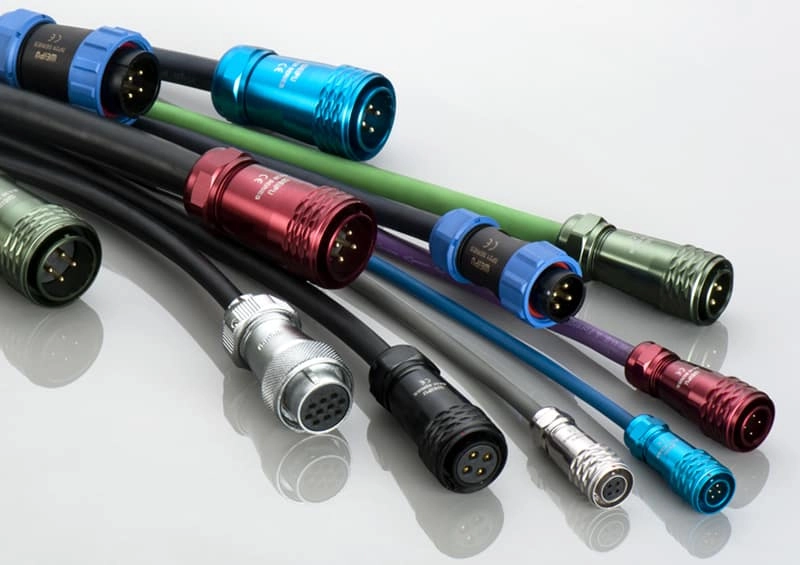
Everything You Need to Know About Cable Connectors
How Circular Connector Manufacturers Meet High-Precision Standards for Medical Equipment in 2026

Weipu Connector Innovations: Pioneering Solutions for Modern Communication
Contacts
Sofia
WhatsApp/Phone

SY1110/P SY1110/S Cable connector IP67
Mate with SP1111,SP1112

WEIPU SP1110P/S Cable Connector IP68
Mate with SP1111, SP1112
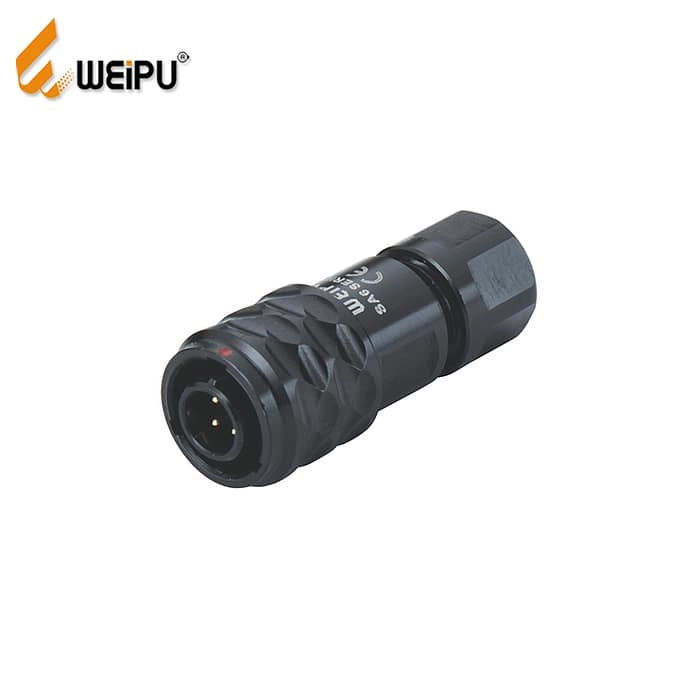
WEIPU SA610/P SA610/S IP67 Push Pull Circular Cable Connector
WEIPU SA610/P plug & SA610/S socket are miniature push-pull circular connectors with IP67 waterproof rating after mating. Built with anodized aluminum shell and gold-plated solder contacts, this SA series supports 2-5 pins, rated 3A 30V, certified CE & RoHS. Ideal for medical diagnostic devices, lab automation and precision sensors, fully compatible with SA611, SA612 and SA615 panel receptacles. WEIPU holds IATF16949 certification and supplies industrial connectors to 130+ countries.

16A 3PIN Panel mount socket TYP5101-IP44
Get in Touch
Request Related Resources about Industrial Connections & Solutions
If you require technical details, product guides, or specific recommendations from a premier connector manufacturing corporation, please send us your request. We provide expert support for custom electrical connectors, offering OEM/ODM customization and dedicated distributor cooperation assistance.
Weipu Building, No. 111, Baihua Road, Liwan District, Guangzhou, Guangdong China
© 2026 WEIPU. All Rights Reserved.
Whatsapp: +8618102298073
WEIPU
WEIPU
WEIPU
WEIPU