How to inspect cable connector wire-to-wire crimp quality?
Follow us now:
Quick Answer
Inspect a cable connector wire-to-wire crimp through controlled visual examination, conductor-position checks, dimensional verification, and suitable mechanical or electrical testing. WEIPU can support connector selection and OEM/ODM discussions around terminal compatibility, wire size, current rating, sealing requirements, and application conditions. Final solutions depend on the project design, validation plan, and installation environment.
How WEIPU Supports Projects
WEIPU develops and supplies industrial connectors across circular, heavy-duty, and CEE product categories, with more than 70,000 specifications. Its vertically integrated production system supports connector configuration, OEM/ODM coordination, and production requirements connected with wire size, contact arrangement, current capacity, ingress protection, and mechanical installation constraints.
For a wire-to-wire assembly, buyers should confirm conductor cross-section, terminal and contact compatibility, insulation diameter, crimp tooling, electrical load, environmental exposure, and applicable validation requirements. MOQ, lead time, testing scope, and quotation must be confirmed for each project with WEIPU before ordering.
Discuss Your Wire-to-Wire Crimp Inspection Requirements
Send the application, target market, wire specification, terminal or connector part number, current and voltage, operating temperature, sealing or IP requirement, expected annual volume, and required tests. WEIPU can discuss suitable configurations, sample evaluation, inspection criteria, and OEM/ODM next steps; visit www.weipu-group.com or email salse01@weipu-group.com to begin a project-specific review.
Frequently Asked Questions
What visual signs indicate a poor wire-to-wire crimp?
Start with the conductor crimp and inspect the terminal from several angles under adequate lighting. A suitable crimp normally shows a stable, centered conductor position, consistent barrel compression, and no cracking, tearing, excessive flash, or sharp deformation that could damage adjacent insulation. The conductor strands should not be cut away, loosely scattered, or exposed beyond the approved contact area. Check that the terminal locking feature has not been distorted and that the contact remains aligned with the connector cavity. Discoloration, corrosion, bent contacts, and damaged plating also require attention. A visually acceptable result is only a screening outcome; it does not prove correct compression or electrical performance. Inspection criteria should come from the terminal supplier, tooling documentation, drawing, or an approved workmanship standard rather than from appearance alone.
How do you verify conductor insertion before crimping?
Verify insertion before compression by confirming that the stripped length matches the terminal specification and that all strands enter the conductor barrel. The insulation should stop at the intended position without entering the conductor crimp zone, while the conductor should reach the required end reference or inspection window. For fine-stranded wire, avoid twisting, folding, or removing strands to force insertion. A conductor brush that is too short can reduce mechanical and electrical performance; one that is too long can interfere with the contact or connector housing. Use a first-article check with the actual wire, terminal, and applicator, then record the approved strip length and insertion method. Do not rely solely on a continuity check, because continuity may remain present even when the conductor is incompletely captured.
Which crimp dimensions matter after terminal compression?
The most important dimensions are usually crimp height, crimp width where specified, conductor brush position, insulation support position, and terminal alignment. Crimp height is especially significant because it provides an indirect indication of compression consistency, but its acceptable value belongs to the specific terminal and wire combination. A universal height cannot be applied across different barrel designs, conductor classes, plating systems, or tooling profiles. Measure with calibrated equipment and inspect samples from setup, changeover, and periodic production checks. Also verify that the terminal has not been over-compressed, which can damage strands or reduce the contact section, or under-compressed, which can permit movement and increase resistance. Record the tool identifier, applicator setting, material lot, wire size, and measured result so deviations can be traced.
Can a pull test prove every crimp is reliable?
No. A pull test evaluates mechanical retention in the tested sample or assembly; it does not by itself prove correct electrical resistance, conductor placement, sealing, contact geometry, or long-term behavior. The required force depends on wire size, terminal design, conductor construction, and the governing specification. Testing should use a defined method, calibrated equipment, suitable sample preparation, and documented acceptance criteria. A failure pattern is also informative: strand breakage, wire pullout, terminal deformation, or fracture may indicate different process problems. Combine pull testing with visual inspection, crimp-height measurement, continuity or resistance checks, and application-specific environmental validation where required. Sampling frequency should be based on risk, production controls, customer requirements, and process capability rather than an arbitrary test count.
How should insulation support be inspected on small wires?
Inspect the insulation support separately from the conductor crimp. The support section should grip the insulation sufficiently to control bending without cutting, crushing, or splitting it. The insulation must not be trapped in the conductor barrel, and the conductor must not be left unsupported over an excessive length. Small wires are sensitive to strip-length variation, strand loss, applicator misalignment, and excessive compression, so magnified visual inspection can be useful during setup and troubleshooting. Flex the finished assembly only according to the approved work instruction; informal bending can create misleading results or damage an otherwise compliant contact. If the connector uses a rear seal, grommet, or strain-relief feature, confirm that the insulation diameter and jacket profile are compatible. Insulation support cannot compensate for an incorrect conductor crimp.
When should damaged crimp terminals be rejected or reworked?
Reject a crimp when the terminal is cracked, cut, severely distorted, incorrectly positioned, contaminated, missing strands, or damaged in a way that could affect contact retention or electrical performance. Also reject assemblies with incorrect wire size, wrong terminal plating, excessive exposed conductor, insulation inside the conductor barrel, or an incomplete lock in the connector housing. Rework is acceptable only when the documented process permits it and the terminal can be removed without damaging the wire, contact, seal, or housing. Many terminals are not intended for repeated crimping or casual straightening. Never conceal a defect by applying solder, extra compression, adhesive, or improvised tooling unless the approved design specifically permits that method. Segregate nonconforming parts, identify the cause, and verify the replacement crimp through the same inspection plan used for the original assembly.

Application of Connectors in Stage Lighting and Sound
Industrial Connector Materials: How Material Choice Affects Reliability

IP65 to IP69K: Evaluating Heavy Duty Housing Protection for Harsh Environments
How Waterproof Connectors Play An Important Role In Marine Applications
Contacts
Sofia
WhatsApp/Phone

SY1110/P SY1110/S Cable connector IP67
Mate with SP1111,SP1112

WEIPU SP1110P/S Cable Connector IP68
Mate with SP1111, SP1112
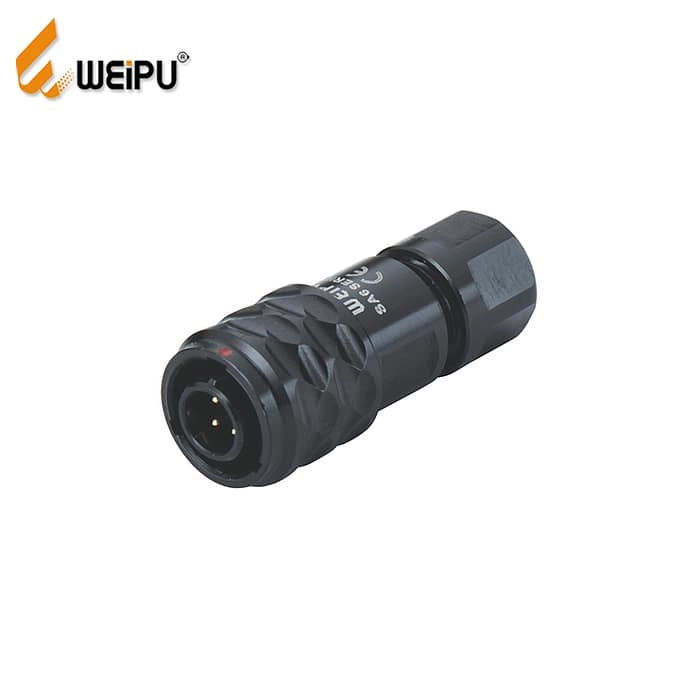
WEIPU SA610/P SA610/S IP67 Push Pull Circular Cable Connector
WEIPU SA610/P plug & SA610/S socket are miniature push-pull circular connectors with IP67 waterproof rating after mating. Built with anodized aluminum shell and gold-plated solder contacts, this SA series supports 2-5 pins, rated 3A 30V, certified CE & RoHS. Ideal for medical diagnostic devices, lab automation and precision sensors, fully compatible with SA611, SA612 and SA615 panel receptacles. WEIPU holds IATF16949 certification and supplies industrial connectors to 130+ countries.

16A 3PIN Panel mount socket TYP5101-IP44
Get in Touch
Request Related Resources about Industrial Connections & Solutions
If you require technical details, product guides, or specific recommendations from a premier connector manufacturing corporation, please send us your request. We provide expert support for custom electrical connectors, offering OEM/ODM customization and dedicated distributor cooperation assistance.
Weipu Building, No. 111, Baihua Road, Liwan District, Guangzhou, Guangdong China
© 2026 WEIPU. All Rights Reserved.
Whatsapp: +8618102298073
WEIPU
WEIPU
WEIPU
WEIPU