How Industrial Connectors Support Machine Vision Systems
Discover how industrial connectors support machine vision systems through reliable power, signal, data, trigger, and control connections. Learn key connector requirements for industrial vision applications.
Follow us now:
- How Industrial Connectors Support Machine Vision Systems
- 1. Where Do Industrial Connectors Fit in a Machine Vision System?
- 2. Camera Connections Require More Than Physical Compatibility
- 3. Lighting Connections Are Also Part of the Vision System
- 4. Trigger Connections Support Timing and Synchronization
- 5. Data Connections Carry the Information the Vision System Needs to Process
- 6. Machine Vision Connectivity Also Includes the PLC and Machine Interface
- 7. Why Connector Reliability Matters in Machine Vision Systems
- Contact Quality
- Locking Mechanism
- Cable Termination
- Mechanical Stability
- 8. Environmental Protection Matters When Vision Moves to the Machine Floor
- 9. EMI and Shielding Can Become Important in Industrial Vision Applications
- 10. What Connector Characteristics Should Engineers Consider?
- Electrical Requirements
- Signal Requirements
- Mechanical Requirements
- Environmental Requirements
- EMC Requirements
- Maintenance Requirements
- 11. Machine Vision Connector Selection Should Follow the Connection Function
- 12. Engineering Example: WEIPU M23 for Machine Vision Connectivity
- 13. A Practical Machine Vision Connectivity Checklist
- Connection Function
- Electrical
- Signal and Data
- Mechanical
- Environment
- Maintenance
- Conclusion
- FAQ
How Industrial Connectors Support Machine Vision Systems
Machine vision systems are often associated with cameras, lenses, lighting and image-processing software.
But a vision system is more than a camera.
Behind every inspection process is a network of physical connections that carries power, image data, trigger signals, lighting control signals and machine-control information.
A simplified machine vision architecture may look like this:
Sensor → Trigger → Camera → Vision Controller → PLC → Machine
At the same time:
Lighting → Power / Control → Vision System
And:
Camera → Data Connection → Industrial Network → Vision Controller / Industrial PC
Every connection point has its own electrical, mechanical and environmental requirements.
This is where industrial connectors become an important part of the machine vision infrastructure.
Industrial connectors do not perform the image processing themselves. Their role is to maintain the physical connections that allow power, signals, data and control information to move reliably through the vision system.
The distinction is important.
A machine vision connector should not be selected simply because it can physically connect a camera or sensor. Engineers also need to consider the type of connection, signal characteristics, locking method, environmental exposure, cable termination and maintenance requirements.
1. Where Do Industrial Connectors Fit in a Machine Vision System?
A typical industrial vision system may contain several interconnected components:
- Industrial cameras
- Vision sensors
- Lighting systems
- Trigger sensors
- Vision controllers
- Industrial PCs
- PLCs
- Industrial Ethernet switches
- Robot controllers
- Production equipment
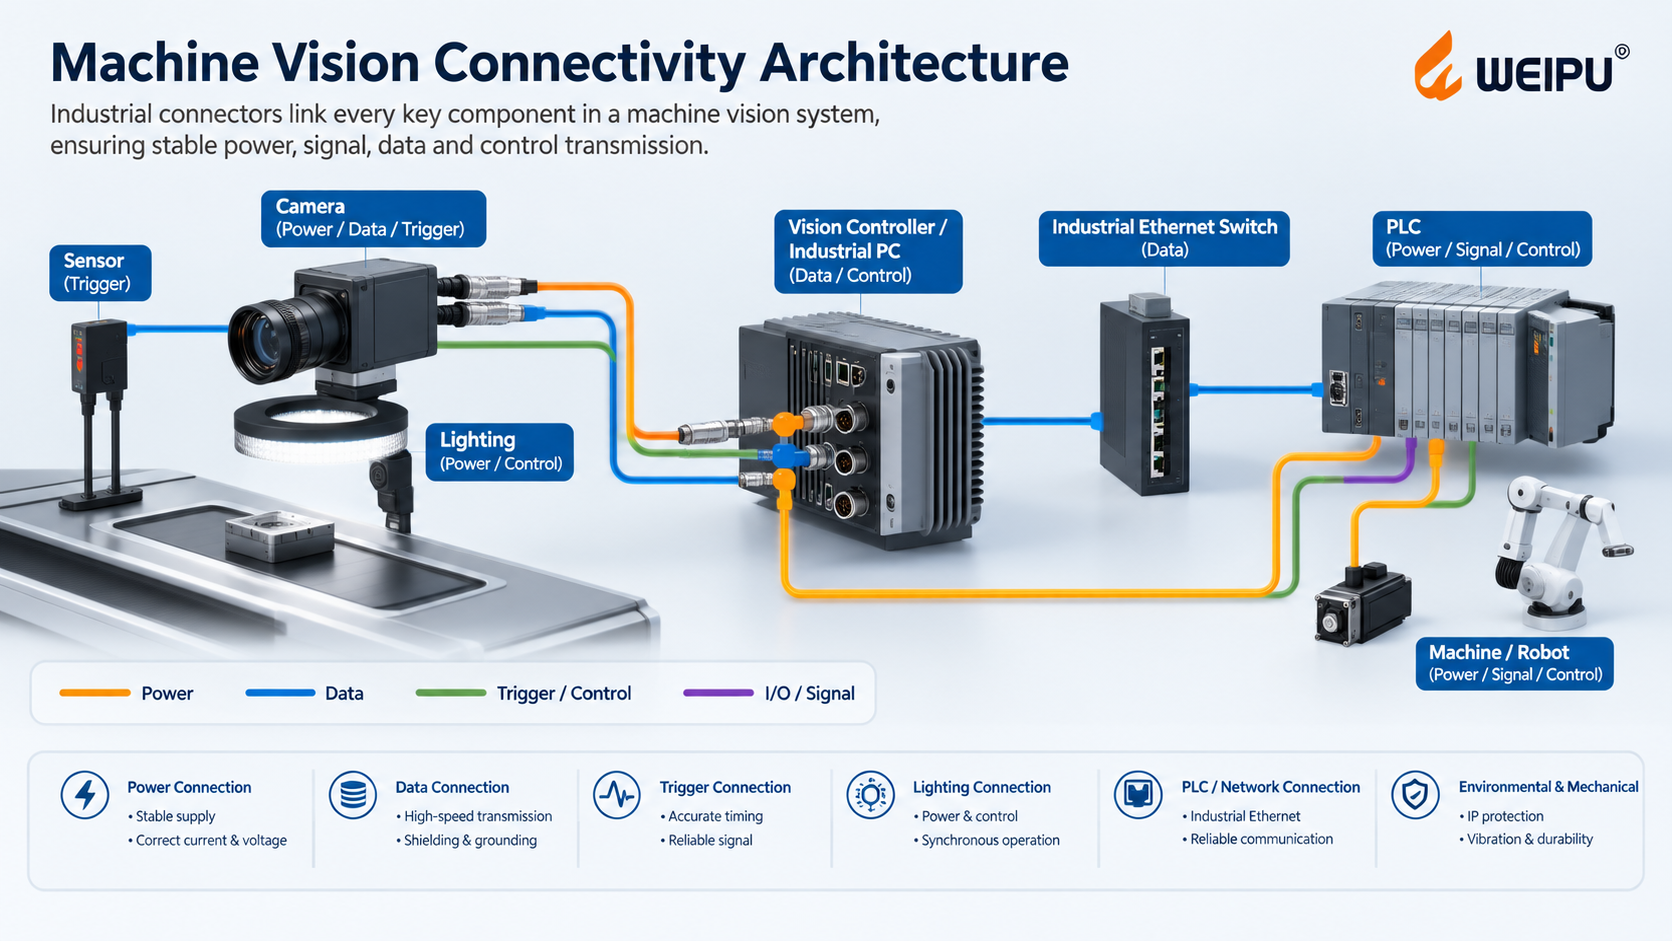
The connector requirements can therefore vary significantly from one connection point to another.
For example:
| Machine Vision Connection | Main Function | Key Connector Considerations |
|---|---|---|
| Camera power | Supply the camera | Voltage, current, contact reliability |
| Camera data | Transfer image data | Signal integrity, shielding, connection stability |
| Trigger | Synchronize image capture | Contact quality, response consistency |
| Lighting | Power and control illumination | Current, switching, environmental protection |
| PLC interface | Exchange control signals | Signal reliability, pin configuration |
| Industrial network | Transfer system data | Data performance, shielding, grounding |
| Machine interface | Connect vision results to equipment | Power, signal, mechanical reliability |
This means there is no single “machine vision connector” that automatically fits every part of the system.
The connector should be selected according to what the connection carries and where it operates.
2. Camera Connections Require More Than Physical Compatibility
The camera is usually the most visible connection point in a machine vision system.
A camera may require separate or combined connections for:
- Power
- Image data
- Trigger signals
- Control signals
The physical connection therefore becomes part of the camera's operating infrastructure.
For camera power, engineers need to consider the required voltage, current, contact configuration and cable specification.
For image data, additional considerations may include:
- Signal integrity
- Shielding
- Grounding
- Cable termination
- Connector structure
- Mechanical stability
A connector that remains physically secure but introduces an unstable electrical interface can still become a weak point in the system.
This is why camera connectivity should be evaluated as:
Camera + Cable + Connector + Processing Equipment
rather than treating the connector as an isolated component.
3. Lighting Connections Are Also Part of the Vision System
Lighting is fundamental to machine vision because image quality depends heavily on how consistently the target is illuminated.
However, lighting is sometimes treated as separate from the connectivity architecture.
In practice, industrial vision lighting can require connections for:
- Power
- Triggering
- Control
- Synchronization
For example, a camera may capture an image only when a trigger signal is received, while the lighting system must provide the correct illumination at the corresponding moment.
This creates a simple but important chain:
Object Detection → Trigger → Lighting → Camera Capture
A connection problem at any point can interfere with the intended sequence.
Industrial connectors supporting lighting equipment therefore need to be evaluated according to the electrical load, switching conditions, installation environment and required service life.
This is one reason why machine vision connectivity should not be reduced to camera-to-computer data transmission.
The complete system contains multiple electrical interfaces.
4. Trigger Connections Support Timing and Synchronization
Trigger signals are another important connection within machine vision systems.
A trigger may come from:
- Photoelectric sensors
- Proximity sensors
- Encoders
- PLC outputs
- Motion-control systems
- Other machine-control devices
The trigger tells the vision system when an image should be captured or when another operation should occur.
In a production line, this can be part of a larger sequence:
Sensor Detection → Trigger Signal → Camera Capture → Image Processing → PLC Decision → Machine Action
The connector is part of the physical path carrying these signals.
For trigger and control connections, engineers should consider:
- Contact reliability
- Pin configuration
- Cable termination
- Locking mechanism
- Vibration
- Environmental exposure
The goal is not simply to establish electrical continuity once.
The connection should remain stable throughout repeated machine operation.
5. Data Connections Carry the Information the Vision System Needs to Process
Modern machine vision systems can generate significant amounts of image and control data.
A simplified path may be:
Camera → Connector → Cable → Network → Industrial PC / Vision Controller
The connection must maintain the physical conditions required for reliable data transmission.
Important factors include:
- Contact quality
- Connector structure
- Cable compatibility
- Shielding
- Grounding
- Mechanical stability
- Environmental protection
A connector does not process the image data, but it forms part of the physical transmission path.
That makes connector reliability relevant to the overall data path.
For machine vision systems operating near motors, servo drives or other potential EMI sources, shielding and grounding may also become important considerations.
6. Machine Vision Connectivity Also Includes the PLC and Machine Interface
A machine vision system rarely operates independently.
After an image is processed, the result may need to be communicated to:
- PLCs
- Robot controllers
- Motion controllers
- Actuators
- Sorting equipment
- Production-line control systems
For example:
Camera → Vision Controller → PLC → Actuator
The camera side may prioritize image data, while the machine interface may carry discrete control signals or other information.
This creates different connector requirements within the same vision application.
The connection between the vision system and PLC can therefore be considered part of the wider automation architecture.
This is closely related to the role of industrial connectors in PLC systems:
Industrial Connectors for PLC Systems: Power, Signal, Data and Reliability
The important principle is:
Machine vision connectivity does not stop at the camera. It extends from the sensing point to the machine-control interface.
7. Why Connector Reliability Matters in Machine Vision Systems
Although this is not primarily an “inspection accuracy” article, connector reliability remains important because the vision system depends on continuous physical connectivity.
Several connector characteristics can influence system stability.
Contact Quality
Stable contacts help maintain consistent electrical continuity.
Poor contact conditions can contribute to intermittent signals or communication interruptions.
Locking Mechanism
Machine vision equipment may be installed on:
- Production lines
- Robotic cells
- Moving equipment
- CNC machines
- Automated inspection stations
A suitable locking mechanism can help maintain the connection under expected vibration and movement.
Common locking approaches include:
- Push-pull
- Threaded coupling
- Bayonet
- Lever locking
The appropriate mechanism depends on the application.
Cable Termination
The connection between the cable and connector is another potential weak point.
Engineers should consider:
- Crimping
- Soldering
- Cable size
- Strain relief
- Shield termination
- Installation method
The connector and cable should therefore be evaluated as a complete assembly.
Mechanical Stability
Repeated vibration or movement can place stress on:
- Contacts
- Cable termination
- Connector locking structures
- Cable entry points
This is particularly relevant for robotic and dynamic vision applications.
8. Environmental Protection Matters When Vision Moves to the Machine Floor
A camera installed inside a protected inspection cabinet has different environmental requirements from one installed directly on production equipment.
Machine vision equipment may encounter:
- Dust
- Moisture
- Oil
- Coolant
- Cleaning processes
- Temperature changes
- Mechanical vibration
When connectors are exposed to these conditions, environmental protection becomes part of the connection design.
The required IP rating should be determined by the actual installation environment.
For example, IP67 can be appropriate for certain applications requiring protection against dust and temporary water exposure, while other environments may require a different protection level.
The important point is:
The required IP rating should follow the environment, not simply the machine vision application label.
9. EMI and Shielding Can Become Important in Industrial Vision Applications
Machine vision equipment may operate close to:
- Servo motors
- Frequency converters
- Industrial drives
- Switching power supplies
- High-current equipment
- Industrial Ethernet systems
These environments can introduce electromagnetic interference.
For sensitive signals and data connections, engineers may therefore need to consider:
Cable Shield → Connector → Equipment → Grounding
The connector should support the intended shielding and grounding architecture when the application requires it.
However, an important engineering distinction should be maintained:
A metal connector housing alone does not automatically make a connector an EMI-shielded solution.
Shielding effectiveness depends on the complete design, including:
- Cable shielding
- Connector configuration
- Shield termination
- Grounding
- Connector structure
- Installation
10. What Connector Characteristics Should Engineers Consider?
Instead of asking only:
“Which connector is suitable for my camera?”
engineers should evaluate the complete connection requirement.
Electrical Requirements
Consider:
- Rated voltage
- Rated current
- Number of contacts
- Contact arrangement
- Cable specification
Signal Requirements
Consider:
- Power
- Digital signal
- Analog signal
- Trigger signal
- Data communication
- Mixed power and signal
Mechanical Requirements
Consider:
- Locking mechanism
- Vibration
- Cable movement
- Mating frequency
- Available installation space
- Mounting method
Environmental Requirements
Consider:
- IP rating
- Temperature
- Moisture
- Dust
- Oil
- Coolant
- Outdoor exposure
EMC Requirements
Where applicable, consider:
- Shielding
- Grounding
- Shield termination
- Connector configuration
- Cable construction
Maintenance Requirements
Finally, consider:
- How frequently the connector will be disconnected
- Whether field replacement is required
- Accessibility
- Cable assembly replacement
- Technician installation time
This approach prevents engineers from selecting a connector based on a single specification while overlooking the rest of the system.
11. Machine Vision Connector Selection Should Follow the Connection Function
Different parts of a machine vision system may require different connector characteristics.
| Connection Point | Primary Requirement | Connector Considerations |
|---|---|---|
| Camera power | Stable electrical supply | Current, voltage, contacts |
| Camera data | Reliable data transmission | Signal integrity, shielding, grounding |
| Trigger | Reliable timing signal | Contact quality, locking |
| Lighting | Power and control | Current, switching, environment |
| Vision sensor | Signal + power | Compactness, IP protection |
| Vision controller | Data + control | Signal integrity, connector interface |
| PLC interface | Control signals | Contact configuration, reliability |
| Robot interface | Dynamic connectivity | Locking, vibration, cable movement |
| Outdoor vision | Environmental protection |
IP rating, material, temperature |
This table illustrates an important principle:
Machine vision does not require one connector specification. It requires a connectivity strategy.
12. Engineering Example: WEIPU M23 for Machine Vision Connectivity
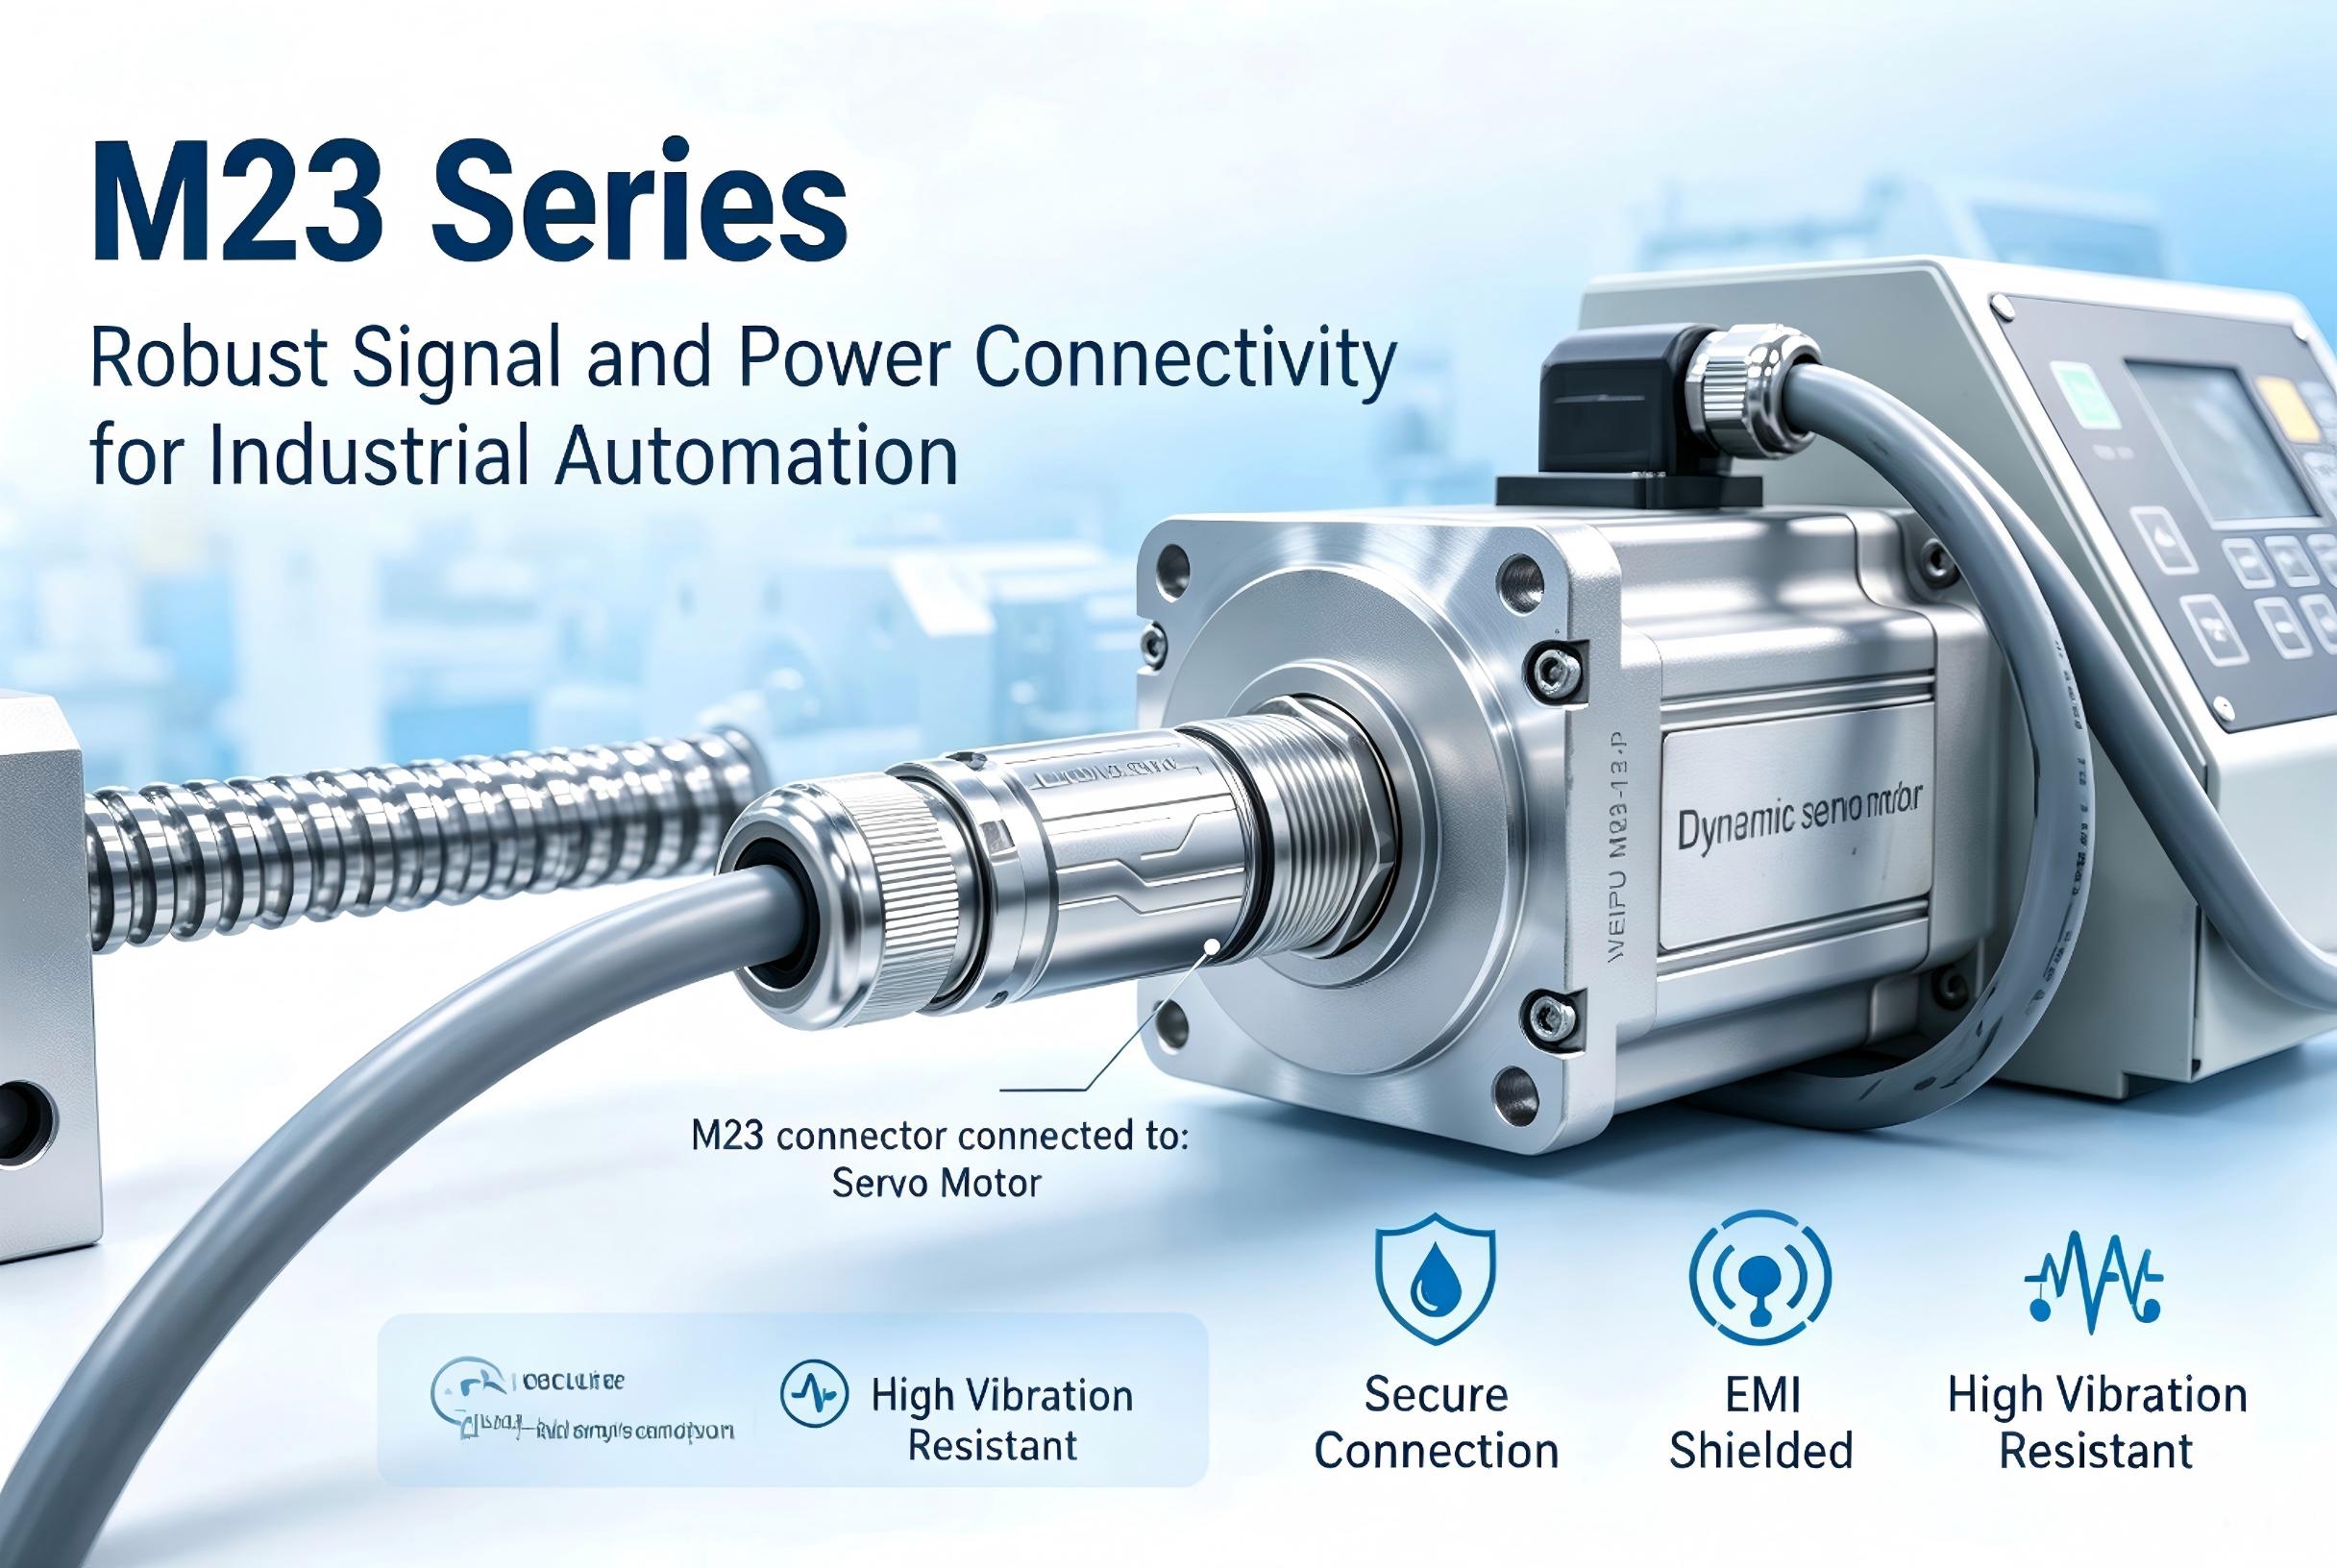
For machine vision systems installed in demanding industrial automation environments, an M23 connector can be considered when robust signal or power connectivity is required.
The WEIPU M23 Series uses threaded coupling and is available in signal and power configurations. The M23 signal range includes configurations designated for shielded and unshielded versions, allowing engineers to consider connector configuration together with cable and EMC requirements. Listed M23 configurations provide IP67 protection and are specified for 1,000 mating cycles, with an operating temperature range of −40°C to +125°C.
For machine vision applications, the M23 Series can therefore serve as an engineering example of robust industrial connectivity, rather than as a universal connector for every camera or vision system.
13. A Practical Machine Vision Connectivity Checklist
Before selecting industrial connectors for a machine vision system, engineers can ask:
Connection Function
Is the connection carrying power, signal, data or a combination?
Is it used for camera, lighting, trigger, PLC or machine interface?
Electrical
What voltage and current are required?
How many contacts are needed?
What cable specification is required?
Signal and Data
Is the signal sensitive to interference?
Is shielding required?
How will the shield be terminated?
Does the connection require stable high-speed data transmission?
Mechanical
Is vibration present?
Will the cable move?
How frequently will the connector be mated?
Which locking mechanism is appropriate?
Environment
Is the connector inside a control cabinet or on the machine?
Is protection from dust or water required?
Is the connector exposed to oil or coolant?
What temperature range is expected?
Maintenance
Will technicians need to disconnect the connector frequently?
Is field replacement required?
Is the connector easy to access?
Can the cable assembly be replaced efficiently?
Conclusion
A machine vision system is not simply a camera connected to a computer.
It is a network of power, signal, trigger, lighting, data and control connections working together across the production environment.
Industrial connectors support this architecture by maintaining the physical interfaces between cameras, sensors, lighting systems, vision controllers, PLCs, networks and machines.
The right connector therefore depends on more than camera compatibility.
Engineers should evaluate:
Connection Function → Electrical Requirements → Signal/Data Requirements → Locking → Environmental Protection → EMC → Mechanical Reliability → Maintenance
This system-level approach helps ensure that connectors are selected according to the actual requirements of the machine vision installation.
Ultimately, reliable machine vision connectivity begins with a simple engineering principle:
Match the connector to the connection, the environment and the system requirement.
FAQ
What types of connectors are used in machine vision systems?
Machine vision systems can use different connector types for camera power, image/data transmission, trigger signals, lighting, PLC interfaces and machine connections. The appropriate connector depends on the electrical, mechanical and environmental requirements of each connection.
What should I consider when selecting a connector for a machine vision camera?
Consider the camera's power requirements, signal or data interface, contact configuration, cable specification, locking mechanism, environmental conditions and any shielding or grounding requirements.
Are industrial connectors important for machine vision systems?
Yes. Connectors form part of the physical infrastructure connecting cameras, sensors, lighting, controllers, PLCs and machines. Reliable connections help maintain stable power, signal and data paths throughout the system.
Do machine vision connectors need IP protection?
Not always. The required IP rating depends on where the connector is installed. A connector inside a protected control cabinet may have different requirements from one mounted directly on machinery exposed to dust, moisture, oil or coolant.
Can M23 connectors be used in machine vision applications?
M23 connectors can be considered for machine vision systems requiring robust industrial signal or power connectivity. WEIPU M23 configurations use threaded coupling, and selected signal configurations are available in shielded and unshielded versions. Application suitability should be evaluated according to the specific electrical, data, mechanical and environmental requirements.
IP65 to IP69K: Evaluating Heavy Duty Housing Protection for Harsh Environments
Industrial Plug: Complete Guide to Types, Standards & How to Choose (2026)
Industrial Connector IP Ratings: How IP67, IP68 and IP69K Affect Application Selection
Hybrid Industrial Connectors: When Power, Signal and Data Share One Connection
Contacts
Sofia
WhatsApp/Phone
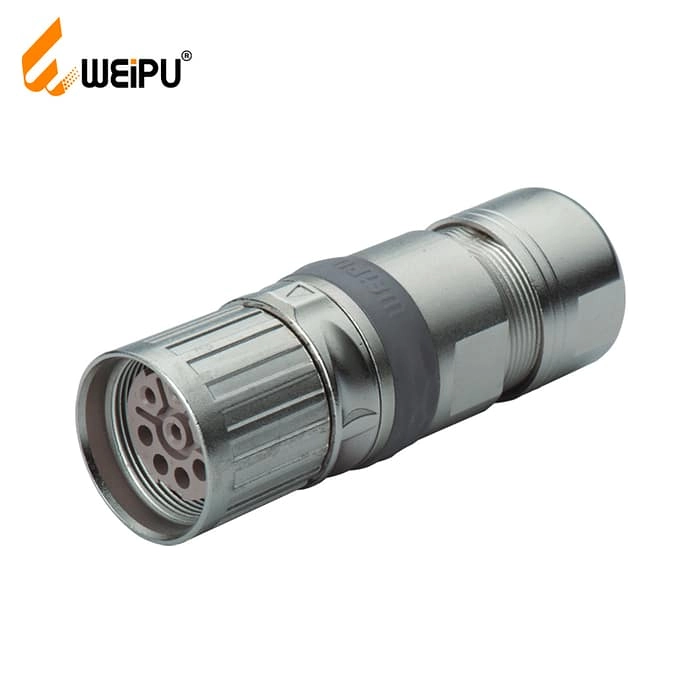
M23DK-TK Female contact cable connector IP67
Mate with M23DJ_TK,M23DK_Z,M23DK_TL,M23DK_ZL
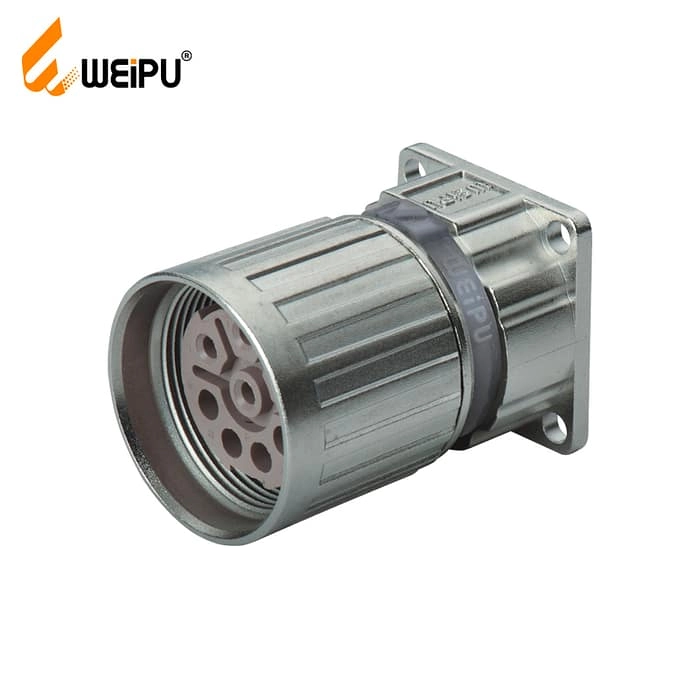
M23DK-Z Female contact square flange receptacle IP67
Mate with M23DJ_TK,M23DJ_TL
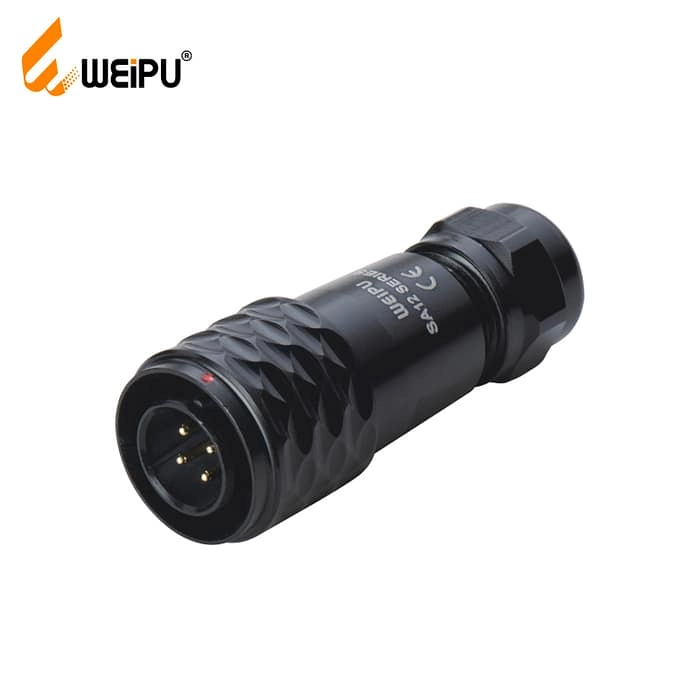
WEIPU SA1210P/S In-line Cable Connector
Weipu’s SA series connectors are meticulously crafted for demanding industrial applications. From marine to medical and automation industries, these connectors excel with their robust aluminum alloy construction and IP67 waterproof rating. With Weipu SA series connectors, you can count on reliable performance and seamless connectivity, ensuring uninterrupted operations in harsh environments.IP67, Mate with SA1211, SA1212, SA1213, SA1215
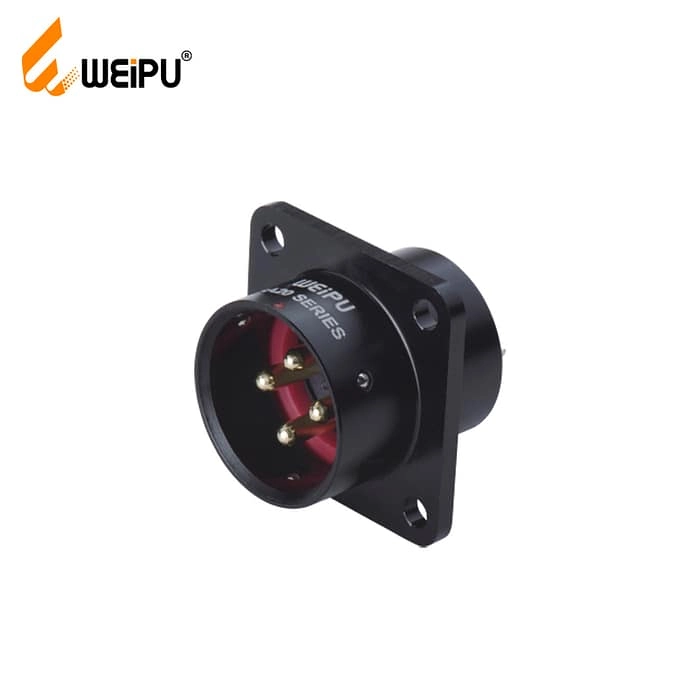
SA2013/P SA2013/S Square flange IP67
Weipu’s SA series connectors are meticulously crafted for demanding industrial applications. From marine to medical and automation industries, these connectors excel with their robust aluminum alloy construction and IP67 waterproof rating. With Weipu SA series connectors, you can count on reliable performance and seamless connectivity, ensuring uninterrupted operations in harsh environments. Mate with SA2010
Get in Touch
Request Related Resources about Industrial Connections & Solutions
If you require technical details, product guides, or specific recommendations from a premier connector manufacturing corporation, please send us your request. We provide expert support for custom electrical connectors, offering OEM/ODM customization and dedicated distributor cooperation assistance.
Weipu Building, No. 111, Baihua Road, Liwan District, Guangzhou, Guangdong China
© 2026 WEIPU. All Rights Reserved.
Whatsapp: +8618102298073
WEIPU
WEIPU
WEIPU
WEIPU